Flax Fibre Fineness and Linear Density Determination Methods
Verify flax linear density using ISO 1973 cut-and-weigh gravimetry at standard 12% regain to accurately forecast wet-spinning limits and enforce contract pricing.
Verify flax linear density using ISO 1973 cut-and-weigh gravimetry at standard 12% regain to accurately forecast wet-spinning limits and enforce contract pricing.
Standardized air permeability methods convert differential pressure across compressed flax plugs into specific surface area to predict spinnable yarn counts.
Accurate gravimetric testing of line flax linear density demands dry mass weighing and standard twelve percent regain adjustment per ISO 6741.
Specify long-staple line flax and wet spinning in purchase contracts to prevent spinners from substituting short tow fibre into ambiguous metric yarn orders.
Commercial mass calculations based on ISO 6741 oven-drying protocols protect buyers from paying landed mass prices on sea-transit moisture uptake in flax.
Multi-spectral optical image analysis of raw flax sliver enables real-time hackling comb adjustments, increasing long line yield by over 7 percent.
Flax fibre grading determines spinnable yarn count, where hackling yield and fibre fineness dictate wet-spinning efficiency and landed cost per metre.
Air permeability testing measures specific surface area to derive bast fibre linear density, requiring precise moisture conditioning and shive removal.
Comb sorter profiling establishes staple length distribution, short fibre content, and drafting bounds to guarantee target yarn counts and fabric yield.
Optical microscopy of resin-embedded cross sections determines true technical flax bundle widths, separating spinnable fine line from coarse drafting defects.
Hot ammonium oxalate extraction isolates calcium-bound middle lamella pectins to quantify sliver spinning limits and drafting cohesion.
Comb array length analysis predicts hackling long-line yield, tow waste, and spinnable count limits to establish true landed cost per finished metre.
Standard moisture regain correction normalizes hackled flax linear density back to twelve percent regain, preventing draw frame drafting errors and financial overpayment.
Verifying flax scutching yield requires dry-mass normalization of input straw against output long fibre, tow, and shive fractions across batch records.
Differentiating line from tow flax in ambiguous quotes requires verifying staple length over 500 mm, shive below 3%, and hackling yields above 50% by contract.
Optimizing hackling pin density and wet-spinning trough temperature stabilizes draft forces, reducing bast yarn end breakage below fifteen breaks per thousand spindle hours.
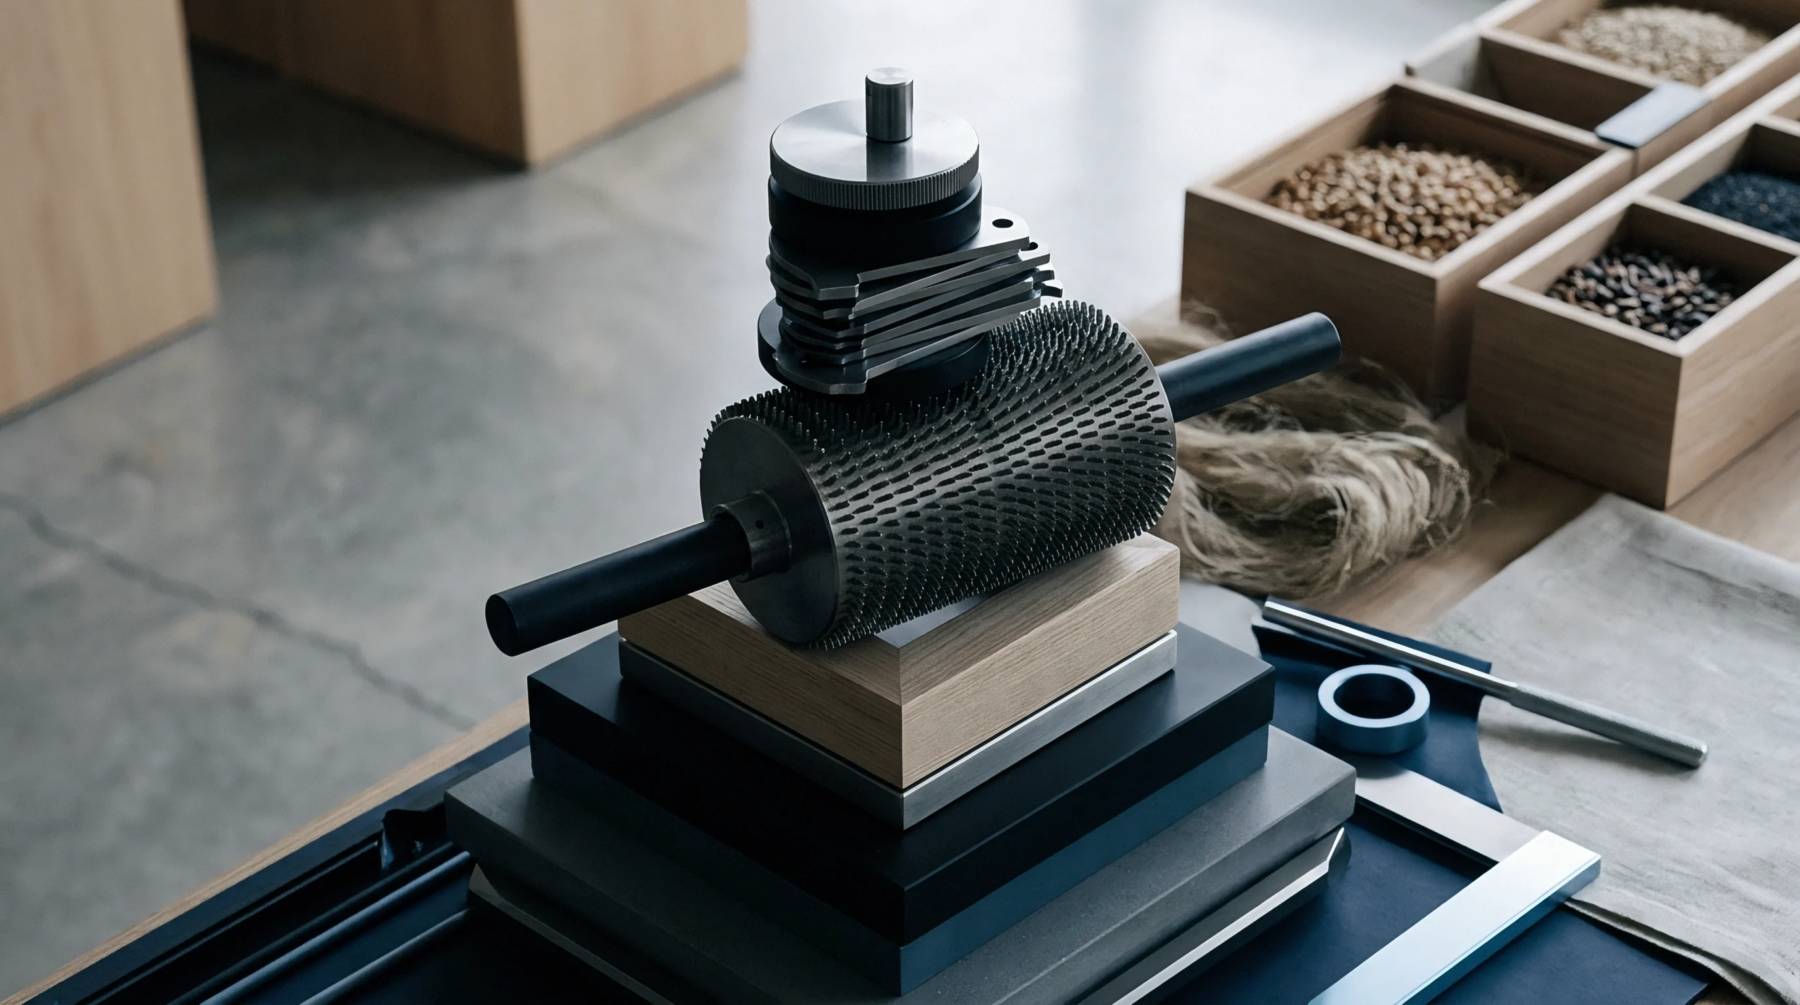
Hackling yield directly establishes net fiber input costs, where a one percent yield gain lowers landed yarn expense by over two percent per finished meter.
Quantifying residual pectins below 1.2% and proteins below 0.75% via spectrophotometry and combustion prevents wet-spinning end breaks and secures high-count Nm yields.
Scutched flax splitting efficiency directly dictates wet-spinning count limits by controlling the distribution of technical bundle diameters prior to roving draft.
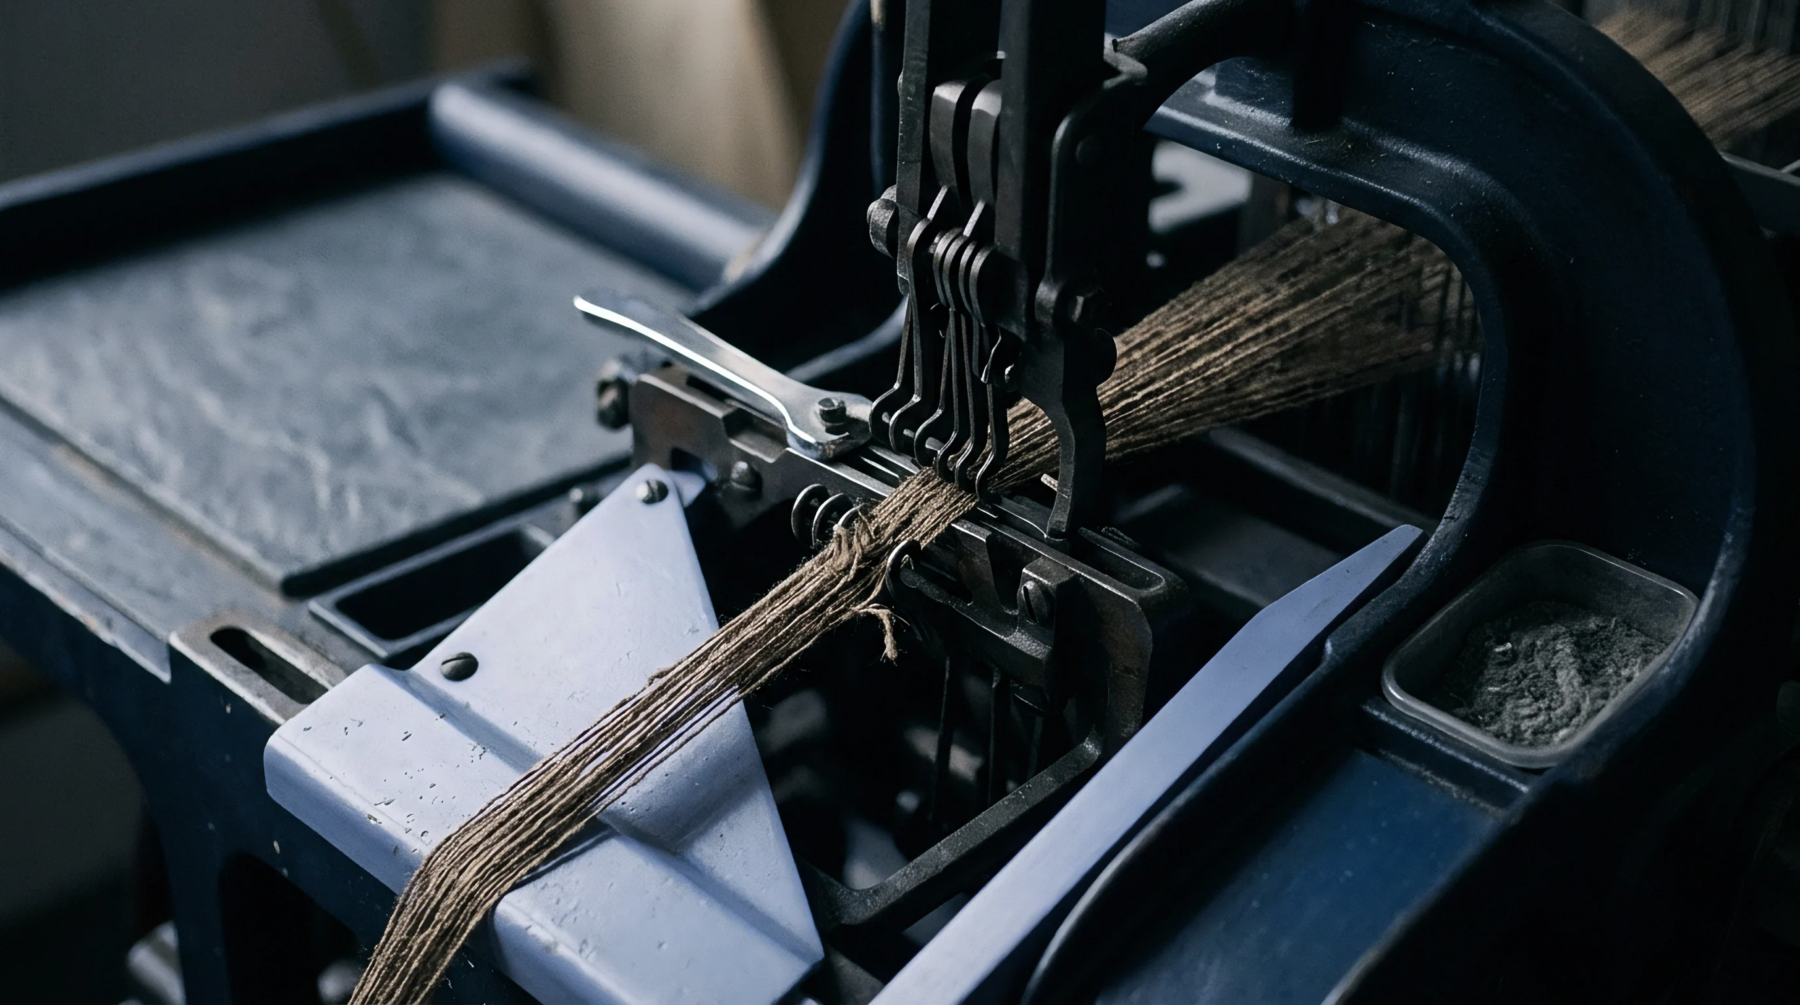
Sliver mass variance generates dynamic force spikes in drafting zones, driving end breaks, reducing frame efficiency, and elevating finished linen yarn costs.
Scutched flax length arrays dictate hackling yield and draft limits, where span length and dispersion metrics set the achievable wet-spun yarn count limit.
Calibrating hackling tool beds within sub-0.05mm tolerances maximizes long-staple line fibre yield, preventing costly stem rupture and securing high-count yarn spinnability.
Flax technical bundle fineness dictates maximum spinnable yarn count while 3.2 millimetre gauge tenacity governs wet-spinning end breaks and hackling yield economics.
Optical sliver grading quantifies shive area and nep density via line-scan arrays to predict wet-spinning end breaks and enforce raw fibre pricing adjustments.
Hydrodynamic shear and hydrothermal pectin dissolution in high-speed wet drafting zones extract 4 to 8 percent of dry flax mass into unmonitored effluent streams.
Residual pectin between 1.3 and 1.8 percent maximizes yarn tenacity by enabling technical bundles to divide for tight packing while preserving axial shear cohesion.
Airflow instruments measure specific surface area to rapidly determine flax bundle metric count, predicting spinning limits and hackling yield.
Controlled decortication moisture and roller clearances prevent fiber wall dislocations that degrade flax tenacity and trigger contractual price rebates.
Cut-and-weigh gravimetric testing on conditioned bundles establishes the baseline tex that determines drafting limits, spinning counts, and invoice weights.
Cross-sectional bundle area distributions dictate wet drafting stress peaks and spinning triangle stability, directly predicting high-speed frame end breakage.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.