Fibre Classification
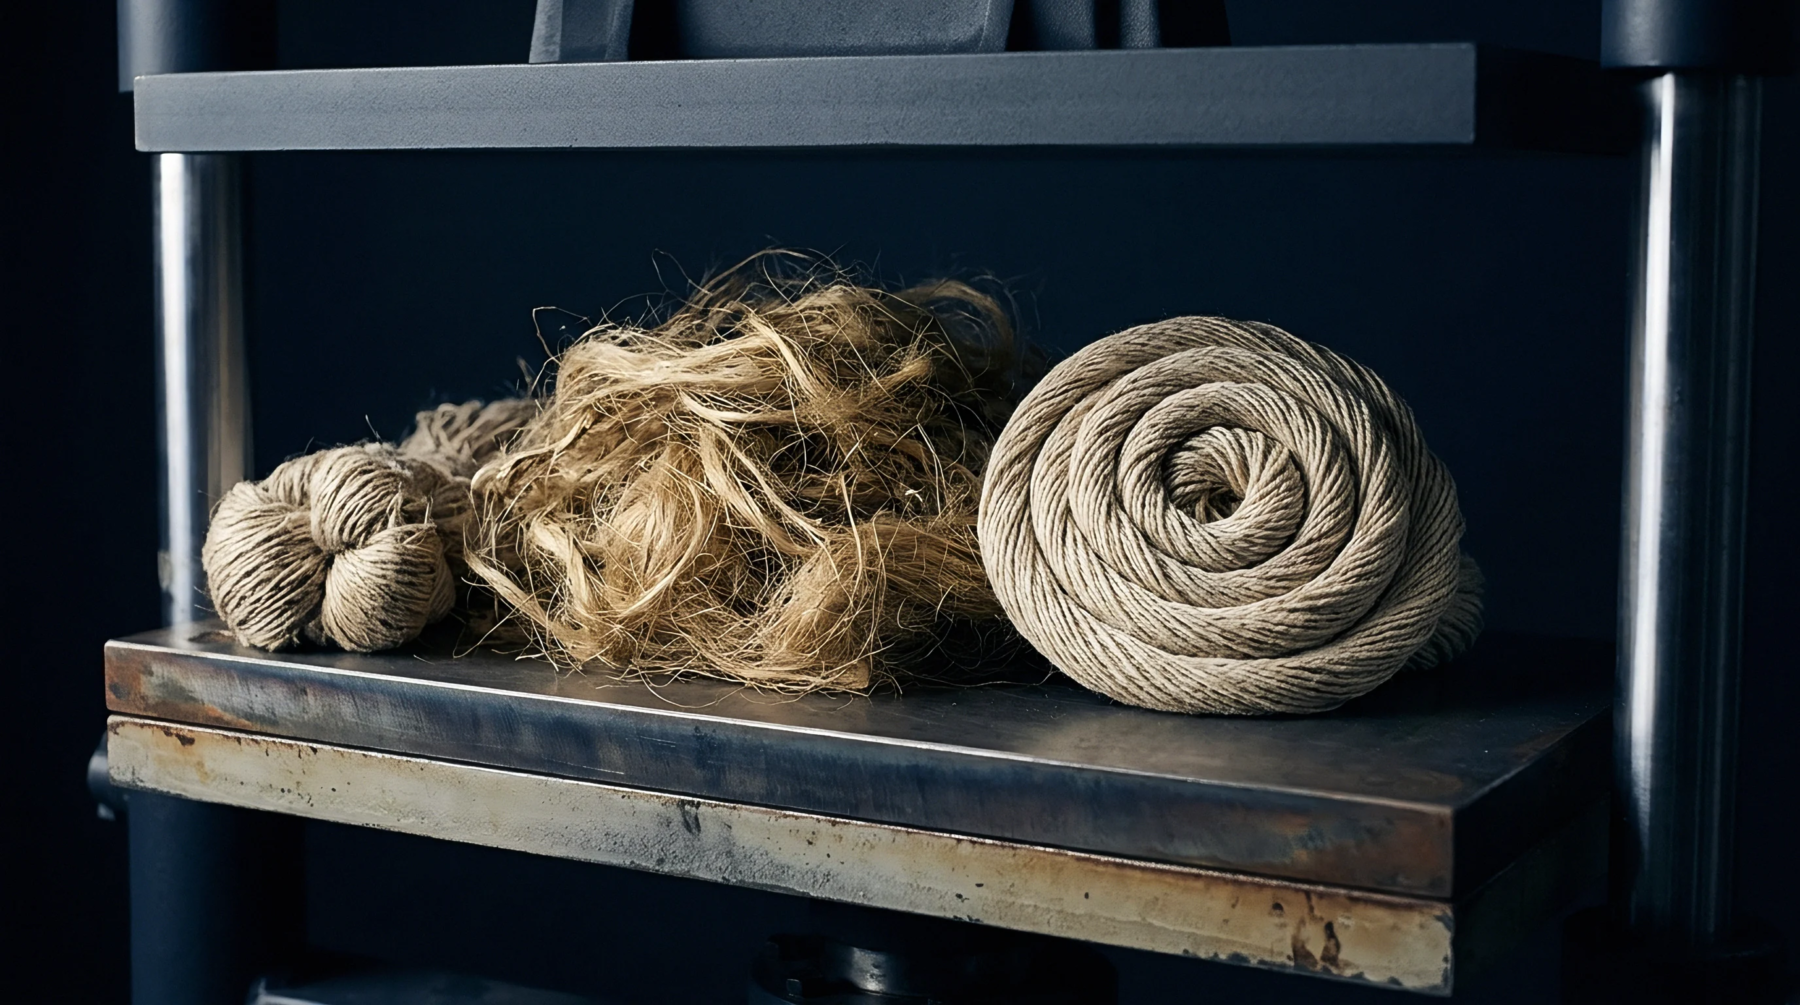
Primary processing of raw flax stalks yields a clean batch of separated bast filaments that the industry classifies as scutched flax. This intermediate material results from mechanical beating that removes woody shives and unwanted vegetable matter from the stem. Mill operators grade the output based on strength, length, and cleanliness, recording the metrics on the packing list before baling for transport.
High quality supply requires minimal residual debris and consistent filament orientation to perform well during subsequent combing operations.
Processing Baseline
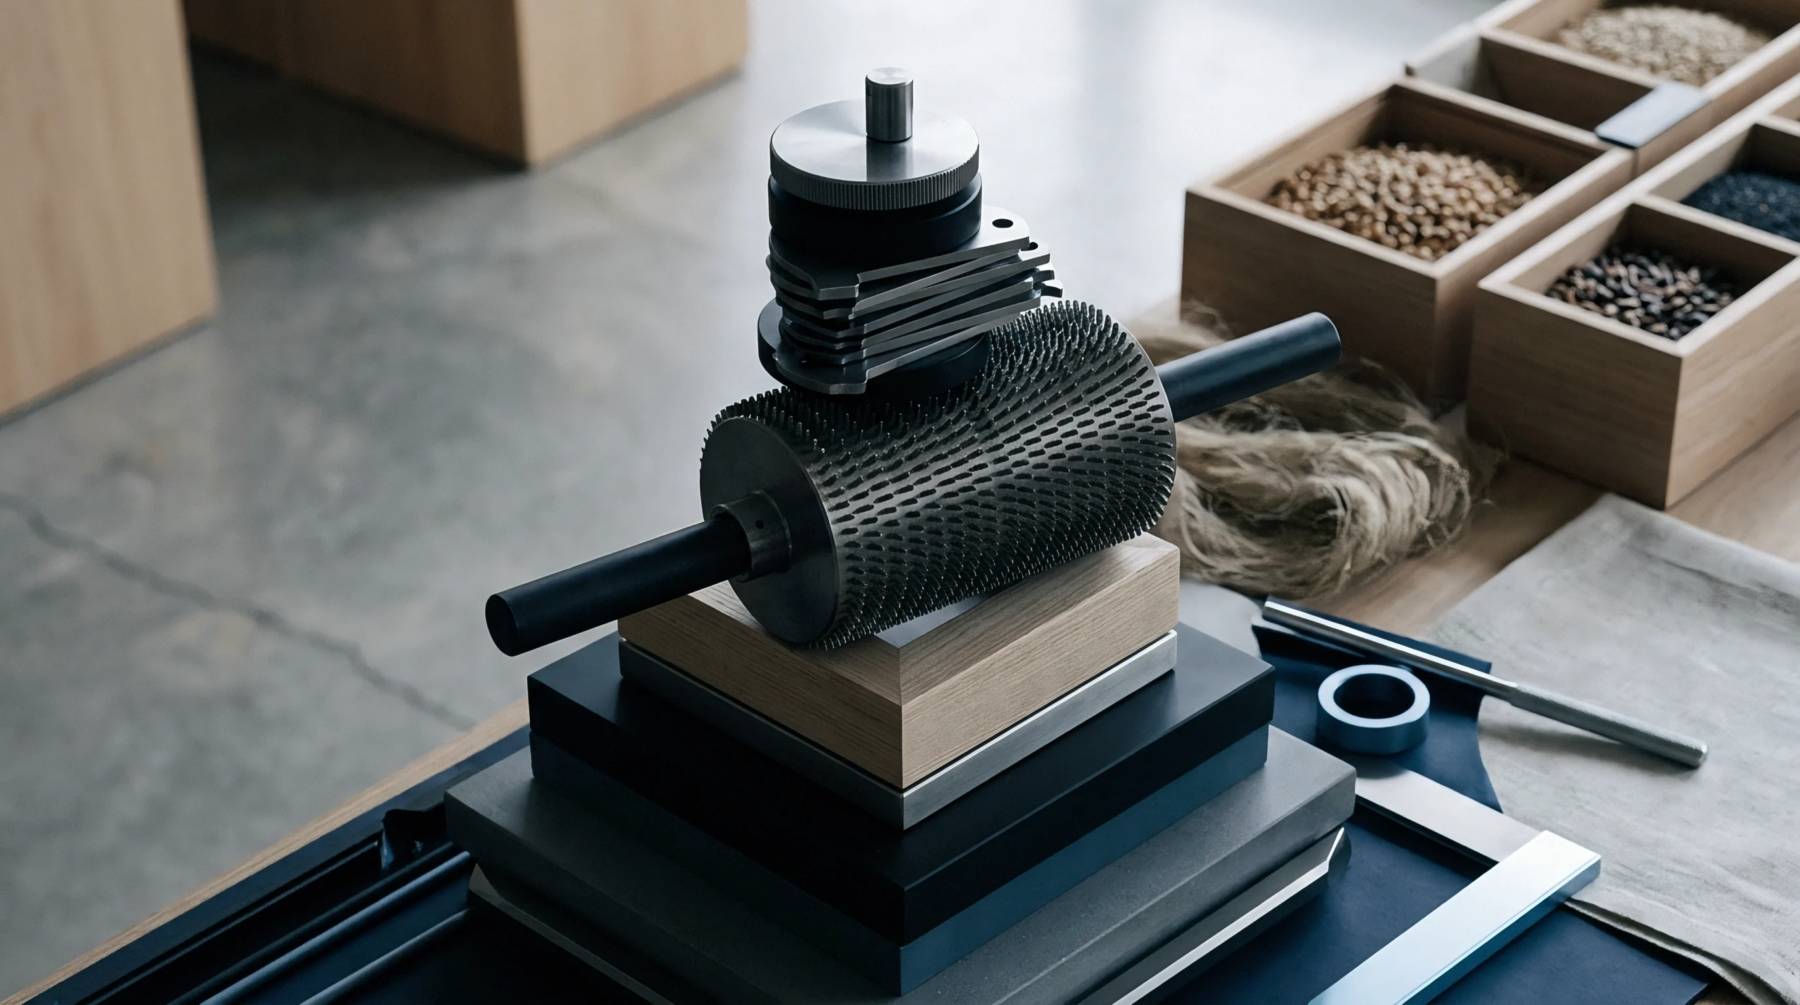
Mechanical decortication involves passing stalk bundles through rotating fluted rollers that break the core while high speed blades clear the pith. Consistency depends on the moisture levels of the stalk and the setting of the scutching turbine gap, where incorrect spacing causes breakage of the long line filaments. Operators monitor these output variations to adjust machinery speed or turbine pressure, ensuring the bale uniformity required by the spinning mill.
Excessive shive retention leads to high waste rates during the subsequent hackling phase, which increases costs and lowers production throughput. Bales reaching the spinning facility undergo verification against the specified grade to confirm they meet the required spinning count. Mills reject batches containing uneven retting or high moisture content because these defects compromise the mechanical stability of the yarn.
Acceptance Criteria
Commercial contracts depend on the cleanliness factor and the average staple length determined by the buyer upon arrival at the mill. Standard purchase agreements define allowable shive percentages, usually measured by weight per hundred kilograms of dry fibre. Suppliers provide samples for testing that determine if the product matches the negotiated grade, as moisture content alters the weight measurement and can mask poor separation quality.
Disagreements arise when the measured length deviates from the initial shipment report, prompting a secondary inspection to verify whether damage occurred during storage or transit. Each delivery must comply with internal mill specifications for spinning consistency, making the accurate classification of this fibre the single biggest factor in the cost efficiency of the output yarn.