Finite Element Modeling of Pectin Lamella Yielding in Fine Linen Weaving
Fine linen warp survival depends on pectin lamella shear limits; FE cohesive zone modeling and 65% RH control prevent inter-fiber slippage under beat-up stress.
Fine linen warp survival depends on pectin lamella shear limits; FE cohesive zone modeling and 65% RH control prevent inter-fiber slippage under beat-up stress.
Mitigate Transaction Certificate latency by tying 15 percent of contract value to certifier registry release and establishing pre-cleared mass balance yields.
Ultrafine linen requires sufficient inter-fiber shear cohesion to resist cyclic shed tension and prevent drafting slip during high-speed cloth production.
Excessive lamella degradation splits line flax prematurely, cutting yarn tenacity below 22 cN/tex and converting high-value line into low-margin hackling tow.
Verifying wet spinning yields requires reconciling dry roving inputs against yarn outputs by measuring trough pectin dissolution and physical waste fractions.
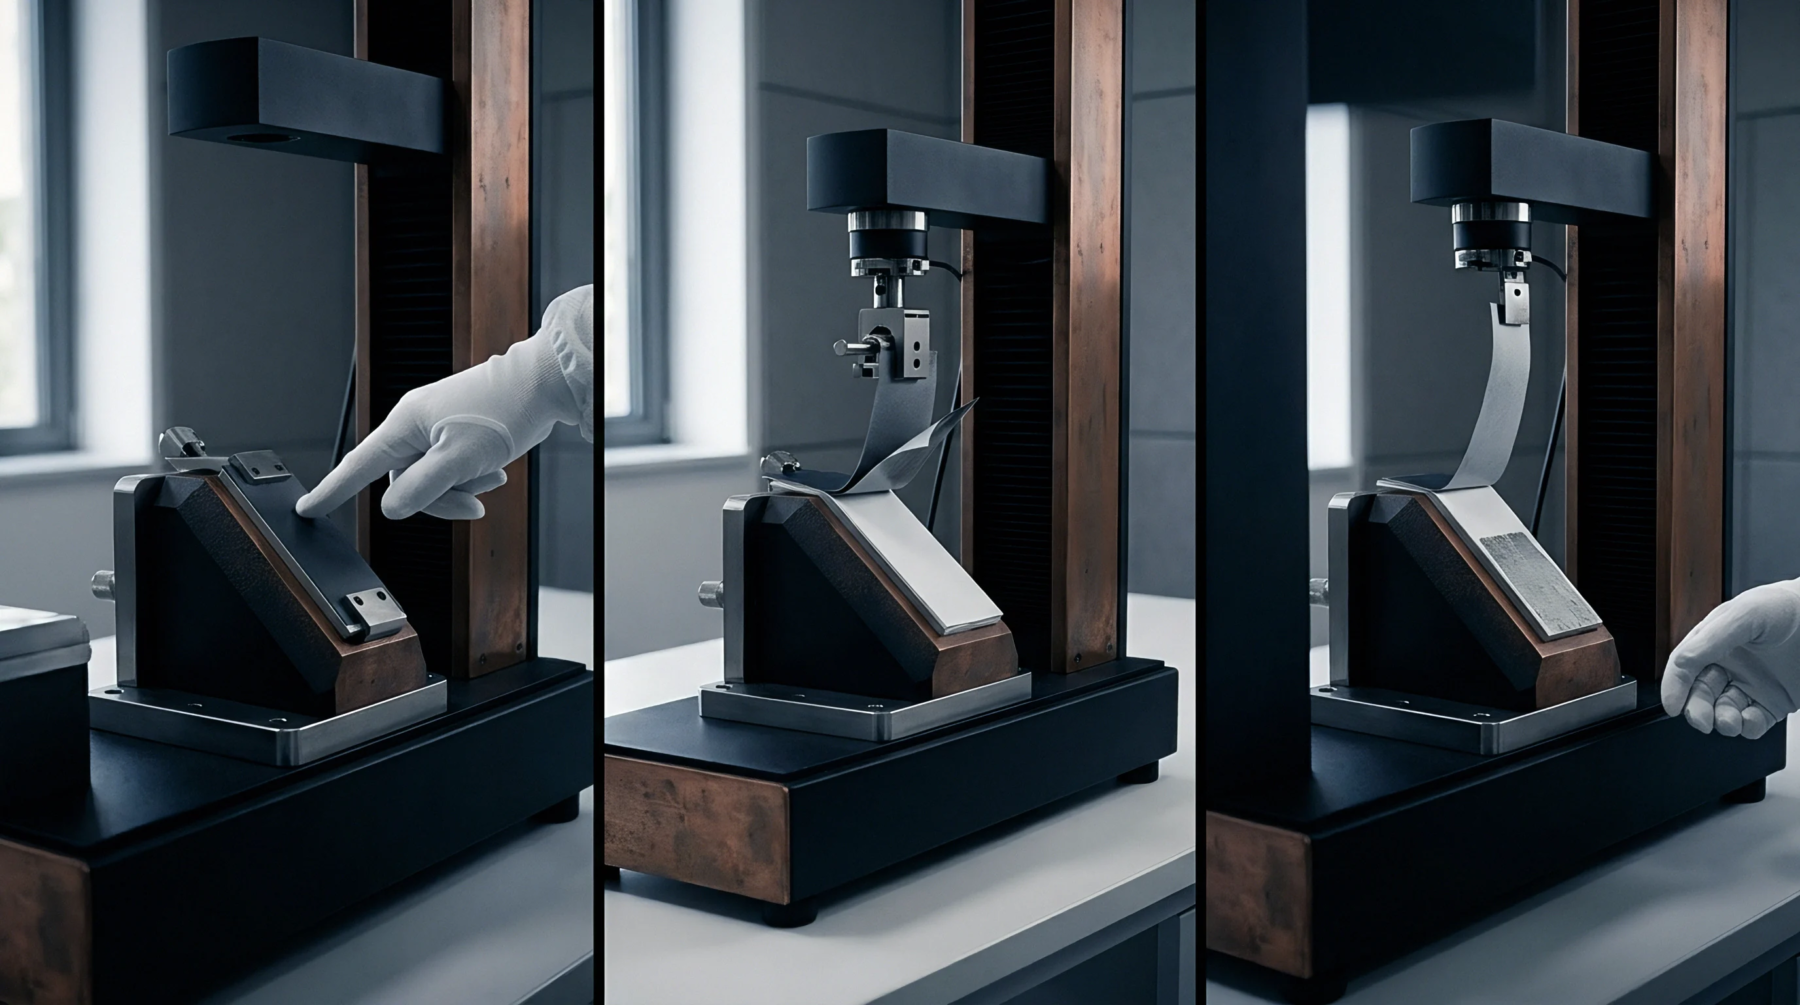
Dynamic oscillatory shed strain in high-count wet-spun flax warps must stay below 1.0 percent to prevent cumulative plastic creep and fatigue breakages.
Enzymatic cleavage splits bast bundles into fine subunits, requiring narrower roller gauges and lower draft ratios to prevent drafting waves in wet spinning.
Targeting residual pectin between 1.8% and 2.6% dry mass optimizes fiber division for Nm 80-100 wet spinning while preventing drafting zone breaks.
Reconciling raw flax intake requires adjusting scale weights to 12% moisture regain, deducting tare, and matching bale tags to transaction certificates.
Active whip roll easing combined with modified starch sizing cuts peak linen warp strain below 3.5 cN/tex, eliminating stop marks and lifting loom efficiency.
Flax hackling yield hinges on sorption history; desorption-path fibers hold higher internal moisture, cutting brittle breakages and shifting line outturn by 3%.
Assessing unaudited toll loomers demands mass-balance checks and machine power audits to prevent uncertified yarn substitution from voiding origin claims.
Reconciling loom capacity with linen greige yield metrics requires cross-referencing digital pick counts, power draws, and mass loss against yarn intake.
Maintain static fine linen warp tension between 8 and 12 percent of single-strand breaking force at 68 percent relative humidity to avert cyclic yarn fatigue.
Non-equilibrium container shipping drives sharp radial moisture gradients in dense flax bales, degrading hackling yield and distorting invoiced fiber weight.
Standard laboratory determination of commercial mass applies fixed moisture regain and extraction allowances to clean dry flax fiber to settle accurate invoice weights.

Model high-density linen contraction by adding off-loom relaxation to aqueous radial fiber swelling to fix reed width, beam length, and loom hours accurately.
Relative humidity during hackling governs pectin plasticization, directly dictating whether gravimetric fineness translates to long line yield or tow waste.
Verifying linen origin demands matching yarn intake lot weights directly to loom pick counters and stamped roll production tallies on the factory floor.
Dew retting pectin breakdown determines hackling yield by reducing middle lamella pin resistance to yield fine line flax while preventing cellulolytic tow waste.
Selecting scutched line flax for high-count wet spinning requires sub-2.2 tex bundle fineness, Pressley tenacity above 6.8, and 12% moisture regain verification.
Non-linear line-scan attenuation mapping resolves bast bundle clustering during high-speed transport to safeguard hackling yields and yarn counts.
Substantial transformation of woven linen requires domestic weaving, leaving importers fully liable for duties and penalties on wet-finished transshipped fabrics.
Modified linen yarns expand effective diameter, requiring open reed setts and lower cover targets to prevent shed jamming and maintain loom efficiency.
Intermediate wet processing converts grey spun linen to finished yarn through non-cellulosic mass loss and chemical add-on that require dry-weight reconciliation.
Linen conversions scale from 1653.5 over Tex while warp jamming occurs where Lea cover factors exceed 18.2 in plain weaves and 23.5 in twills.

Verifying European Flax transaction certificates requires cross checking scope validity dates net invoice weights and multi stage mill conversion rates
Real-time vision-based comb parameter adjustment optimizes pin penetration depth and speed to cut tow generation and maximize long-staple line flax yield.
Statutory foreseeability under CISG Art. 74 limits linen loss recovery to consequences explicitly communicated in technical contract documents before closing.
Dynamic tension balance in fine flax shedding requires low-mass carbon healds, tuned return springs, and reduced shed lift to keep strain spikes under 50 cN.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.