Impact of Dew Retting Pectin Degradation on Hackling Yield and Tow Ratio
Dew retting pectin breakdown determines hackling yield by reducing middle lamella pin resistance to yield fine line flax while preventing cellulolytic tow waste.
Dew retting pectin breakdown determines hackling yield by reducing middle lamella pin resistance to yield fine line flax while preventing cellulolytic tow waste.
Microcracking lowers hackled flax Weibull modulus, expanding tenacity dispersion and multiplying wet-spinning ring breaks despite normal mean bundle strength.
Flax technical bundle fineness dictates maximum spinnable yarn count while 3.2 millimetre gauge tenacity governs wet-spinning end breaks and hackling yield economics.
Commercial claims on enzymatically processed flax require matching residual pectin levels against bundle tenacity and wet-spinning end breakages.
Targeted polygalacturonase retting and controlled 65°C bath chelators depress pectin glass transition, optimizing fine line flax drafting and yarn yields.
Commercial mass adjustments correct landed weight for moisture regain while hackling yield allowances offset long line waste in yarn cost calculations.
Hackling yield directly establishes net fiber input costs, where a one percent yield gain lowers landed yarn expense by over two percent per finished meter.
Raw flax grading requires correlating technical bundle fineness and retting pectin decay with hackling yields to establish wet spinning count limits.
Maintaining residual pectin between 0.8% and 1.4% prevents roving draft collapse while enabling fibre attenuation in wet-spinning ultra-fine linen yarns.
Differentiating line from tow flax in ambiguous quotes requires verifying staple length over 500 mm, shive below 3%, and hackling yields above 50% by contract.
Dry spinning flax intake standards require strict bundle fineness under 2.2 tex, residual shive below 0.8 percent, and 11 percent target moisture regain.
Controlled pectin removal enables clean bundle cleavage, elevating metric fibre fineness above Nm 2000 while maintaining long line yield above 60 percent.
Spectrophotometric galacturonic acid assays overestimate retting degree unless corrected for neutral sugar and phenolic background interference.
Selective pectin degradation paired with tuned hackling pin density maximizes fibre bundle separation while retaining staple length for fine wet spinning.
Flax fibre grading determines spinnable yarn count, where hackling yield and fibre fineness dictate wet-spinning efficiency and landed cost per metre.
Dew retted line flax hackling yield determines long line fiber recovery, tow ratios, and yarn production costs through precise fineness and strength testing.
Optimize wet ring frame trough temperatures to 72°C and hold draft ratios below 17 for Heilongjiang dew-retted line flax to limit end breaks.
Lot-to-lot flax variance costed via hackling yield formulas protects mill margins by adjusting line sliver pricing before wet spinning.
Non-cellulosic content above 3.5% lowers hackling line yield, increasing tow waste and landed line fibre cost per finished metre.
Bale opening routines verify dry mass, bundle tenacity, and shive content under ISO standards to lock in spinnable count and true fibre value before payment.
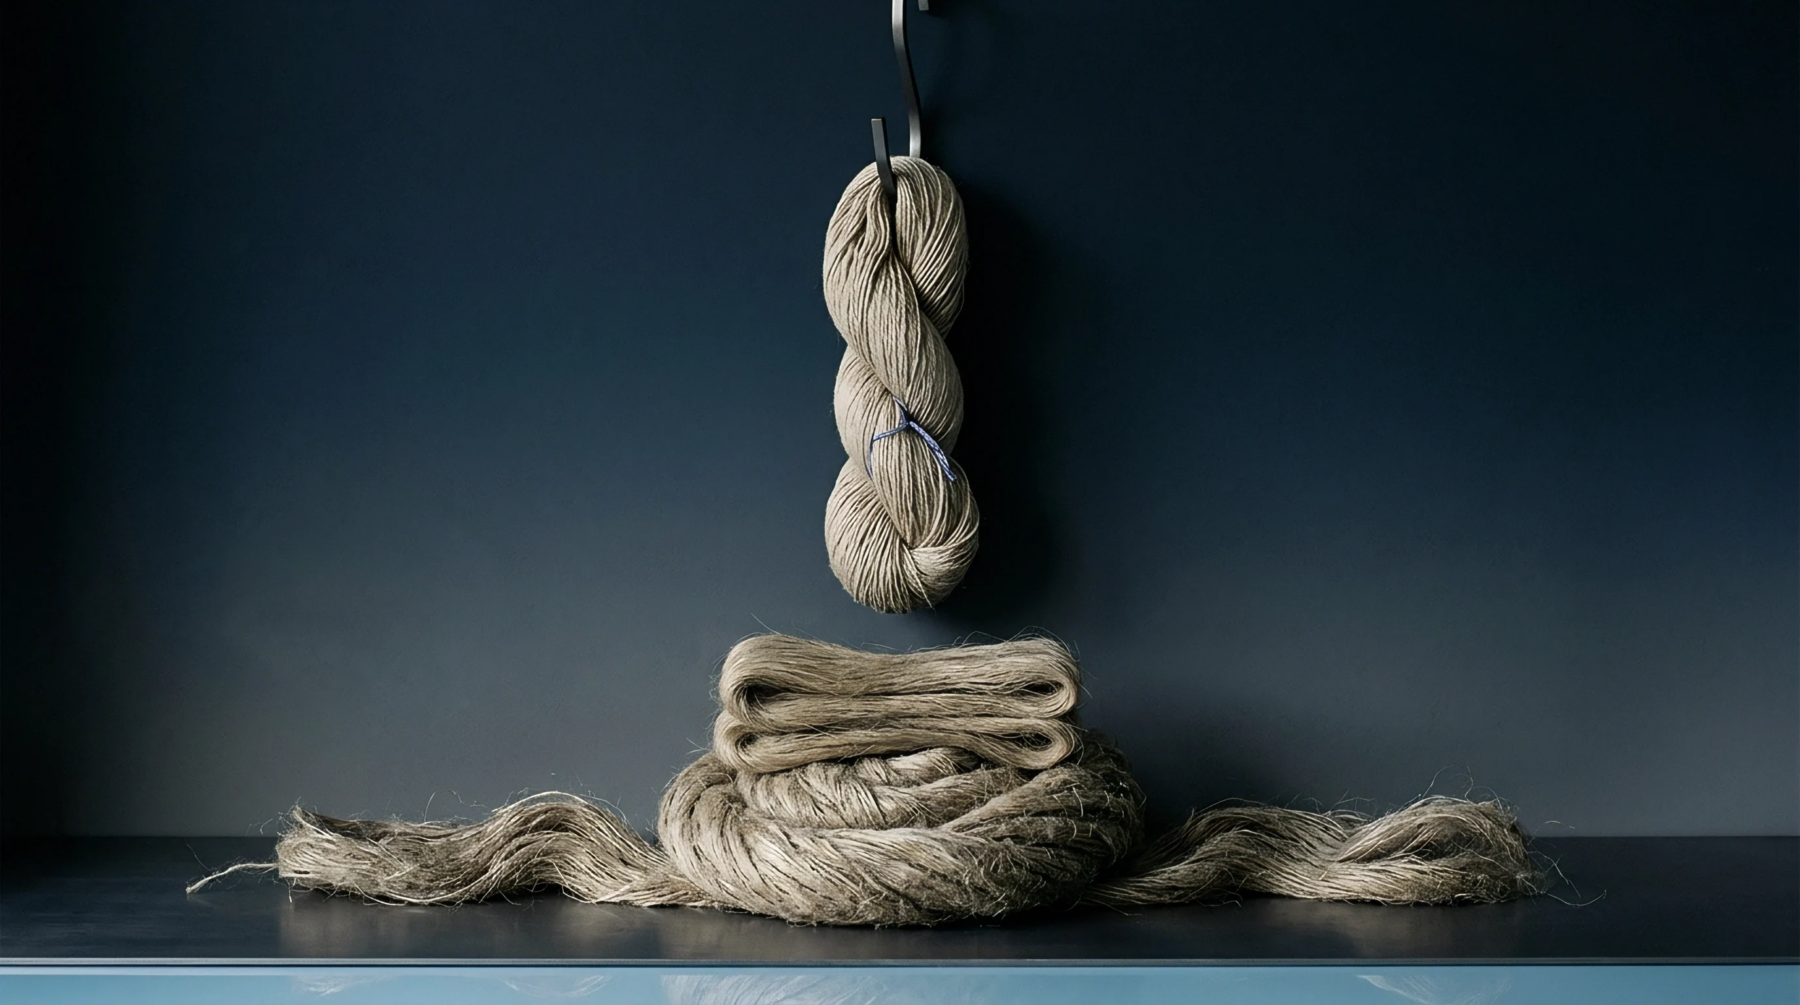
Long staple flax tenacity and scutcher loss dictate yarn spinning limits and processing economics, requiring standardized ISO gauge length testing and mill-level mass balance verification.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.