Discrete Length Distribution Transformations in Bast Fiber Quality Control Protocols
Discrete length distribution transformations control drafting breakage, wet trough bundle dissociation, and finished spinning margins in flax yarn production.
Discrete length distribution transformations control drafting breakage, wet trough bundle dissociation, and finished spinning margins in flax yarn production.
Linear density offsets in long line flax contracts require progressive financial adjustment schedules to offset downstream wet-spinning waste and tenacity losses.
Cut-and-weigh gravimetric testing on conditioned bundles establishes the baseline tex that determines drafting limits, spinning counts, and invoice weights.
Deduct isolated shive mass from cut-length bundle specimens using precision sieving to prevent false linear density coarsening in wet-spinning fineness grades.
Scutcher turbine calibration balances blade clearance and tip speed to strip woody shive while preserving bast bundle tenacity and long line yields.
Controlled decortication moisture and roller clearances prevent fiber wall dislocations that degrade flax tenacity and trigger contractual price rebates.
Sliver cohesion limits wet-spun flax counts by governing technical bundle division into elementary fibres under hot water drafting tension.
Fine wet spun linen above Nm 50 requires 1.35% to 1.85% bound xylan to preserve elementary bundle cohesion and prevent drafting breaks in warm water troughs.
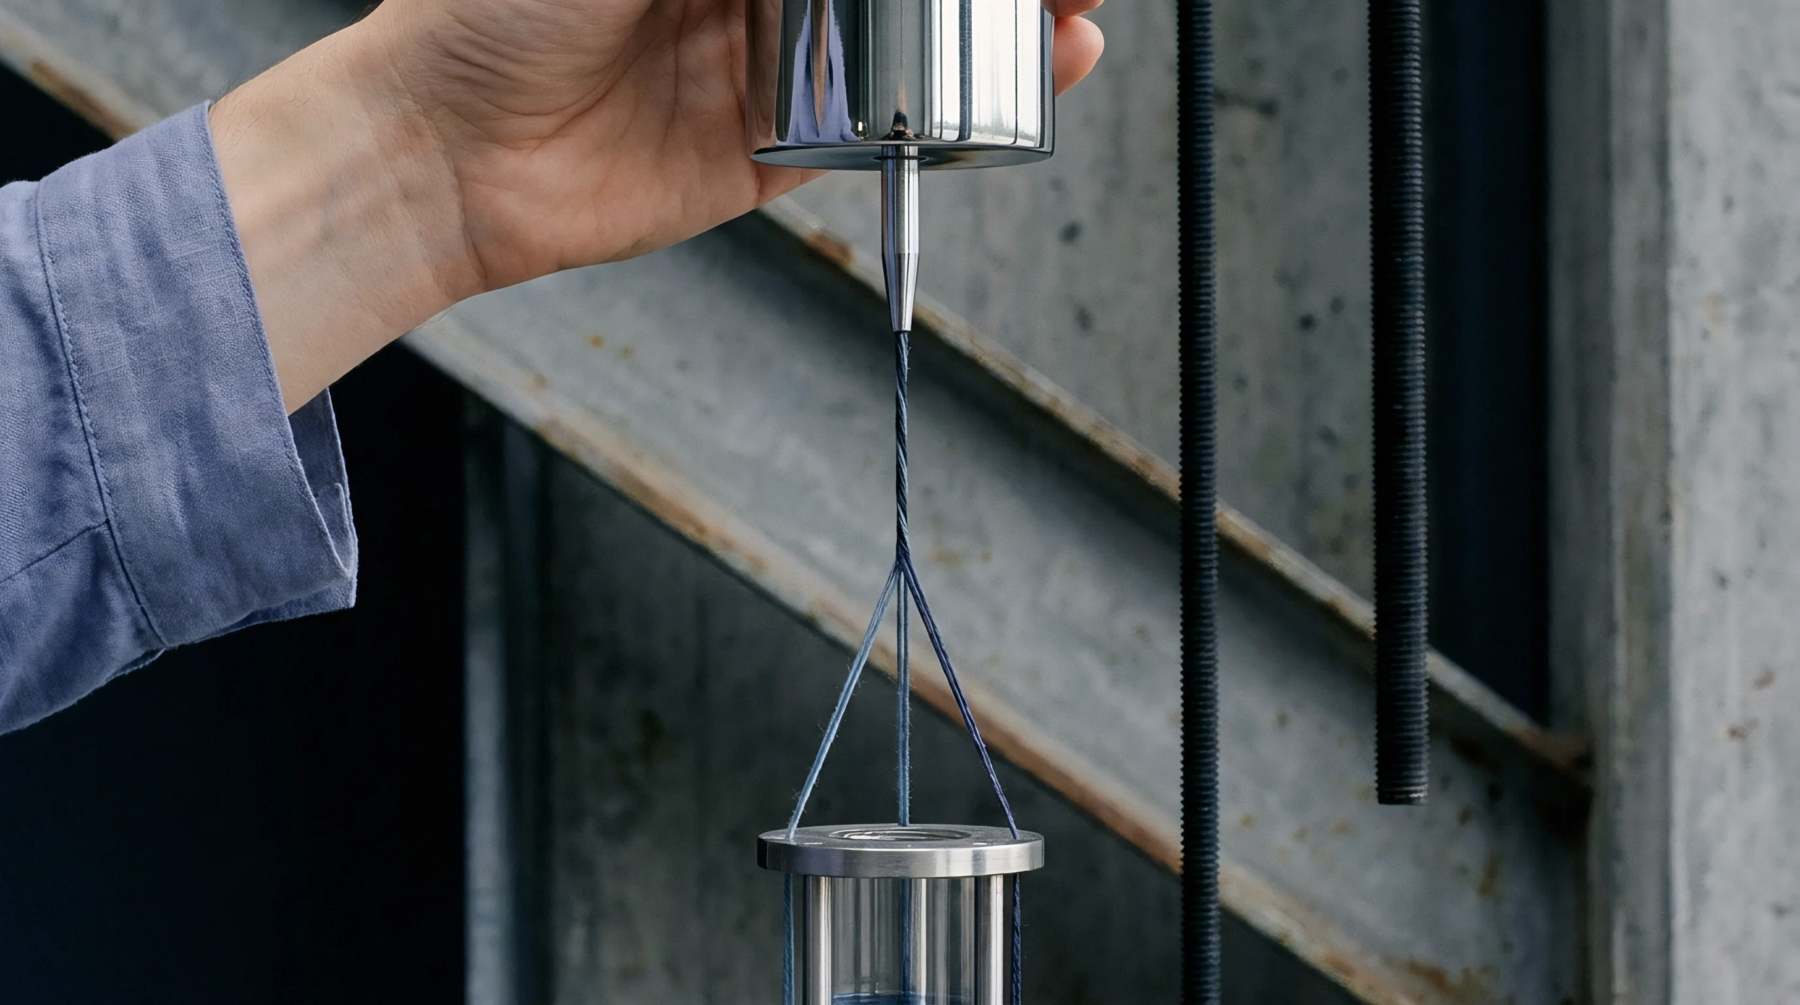
Controlled hot water soaking leaches middle lamella pectins so drafting roller shear divides technical bundles into elementary fibrils without fibre fracture.
Staple length distribution dictates wet spinning limits because unguided short fibers trigger attenuation waves that multiply end breaks and inflate cost per meter
Reconciling hackling yield requires continuous mass balance records matching physical sliver, tow, and extraction waste to incoming scutched flax lot certificates.
Interlaboratory airflow divergence stems from specimen prep and moisture bias, distorting hackling yields and demanding strict referee testing clauses.
Airflow fineness measurement on hackled flax converts pneumatic resistance to metric count, requiring retting-specific calibration to avoid spinning failures.
Uncorrected airflow fineness overstates flax spinnability by measuring collapsed lumen perimeters as external surface area rather than true gravimetric linear mass.
Airflow instruments measure specific surface area to rapidly determine flax bundle metric count, predicting spinning limits and hackling yield.
Scutched flax line classification dictates hackling yield, bundle fineness, and wet-spinning count limits, establishing the landed cost per metre of cloth.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.