Fibre Profile
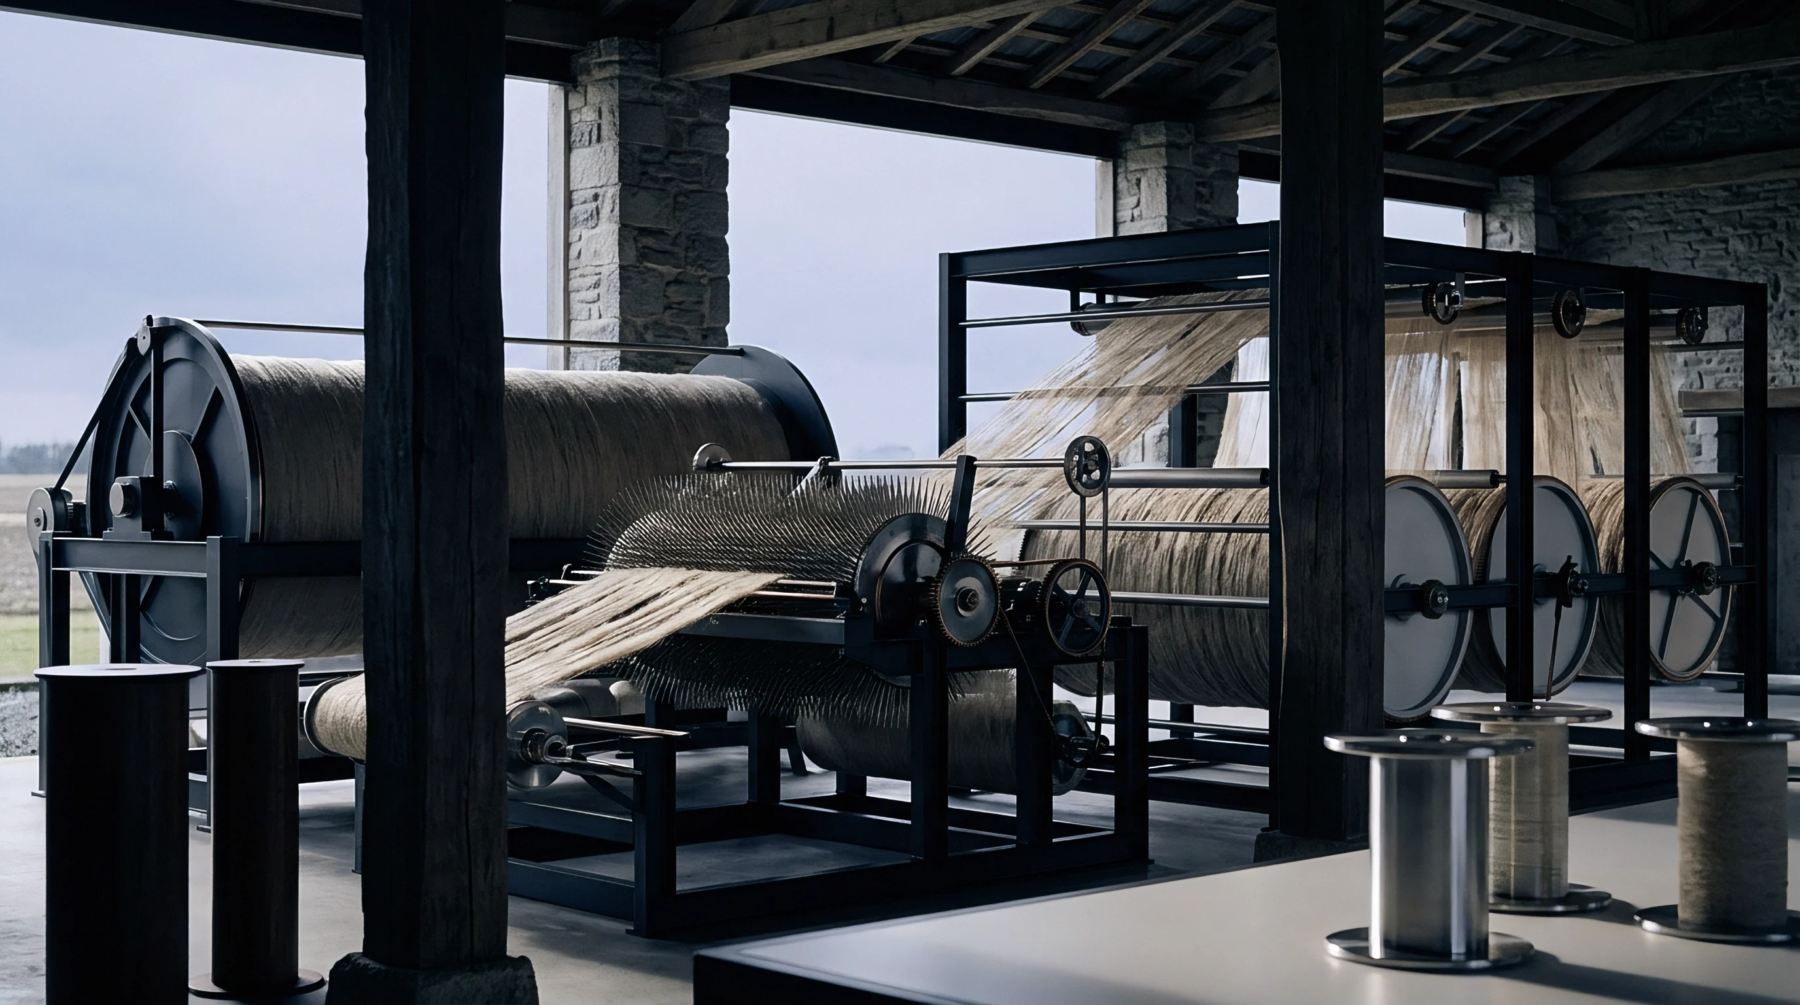
Raw flax material grading relies upon physical measurement procedures to establish batch uniformity before drafting begins. Staple length distribution defines the measured dispersion of individual ultimate filaments within a processed batch, governing the mechanical tension limits during mechanical drawing frames and wet spinning operations. Long drawn filaments demand wider roller settings to prevent fibre breakage, while shorter fractions require tighter spacing to maintain drafting control.
Chinese spinning mills record these dispersion metrics inside the fiber classification dossier accompanying each warehouse bale. Mill technicians distinguish raw fibre grade standards from finished fabric performance thresholds by tracking how short fibre proportions alter yarn hairiness during subsequent ring spinning tasks. Buyer acceptance criteria frequently impose strict tolerance limits on the short fibre index, rejecting batches exceeding specified variance coefficients.
Draft Mechanics
Roller drafting zones require precise geometric adjustments when processing uneven natural cellulose lots. Draft ratios scale directly against the measured dispersion parameters documented in the mill laboratory. High variance batches create drafting waves if roller pressure remains static, forcing operators to modify weighting arms on the intermediate drawing carriages.
Heavy sliver irregularities develop rapidly when short fractions slip prematurely past the nip points before the drafting apron restrains them. Finer yarn counts demand highly uniform fiber populations to prevent episodic breakage peaks on the spinning frames. Production controllers adjust twist multipliers upward when processing lots containing elevated short fibre percentages, compensating for reduced frictional contact between adjacent filaments.
Export Parameters
Finished linen yarn packages undergo rigorous physical testing before clearing customs documentation for international trade. Export grade sheets mandate specific dispersion ceilings to guarantee fabric tensile strength during subsequent high speed loom shedding. Commercial contracts link financial penalties directly to out of tolerance dispersion measurements discovered during independent laboratory audits at the port of destination.
Warehouse inspectors verify bale homogeneity against the original mill classification dossier before releasing shipments to freight forwarders. Final export certification depends entirely upon maintaining strict statistical control over raw material preparation stages throughout the manufacturing chain.