Classification Standard
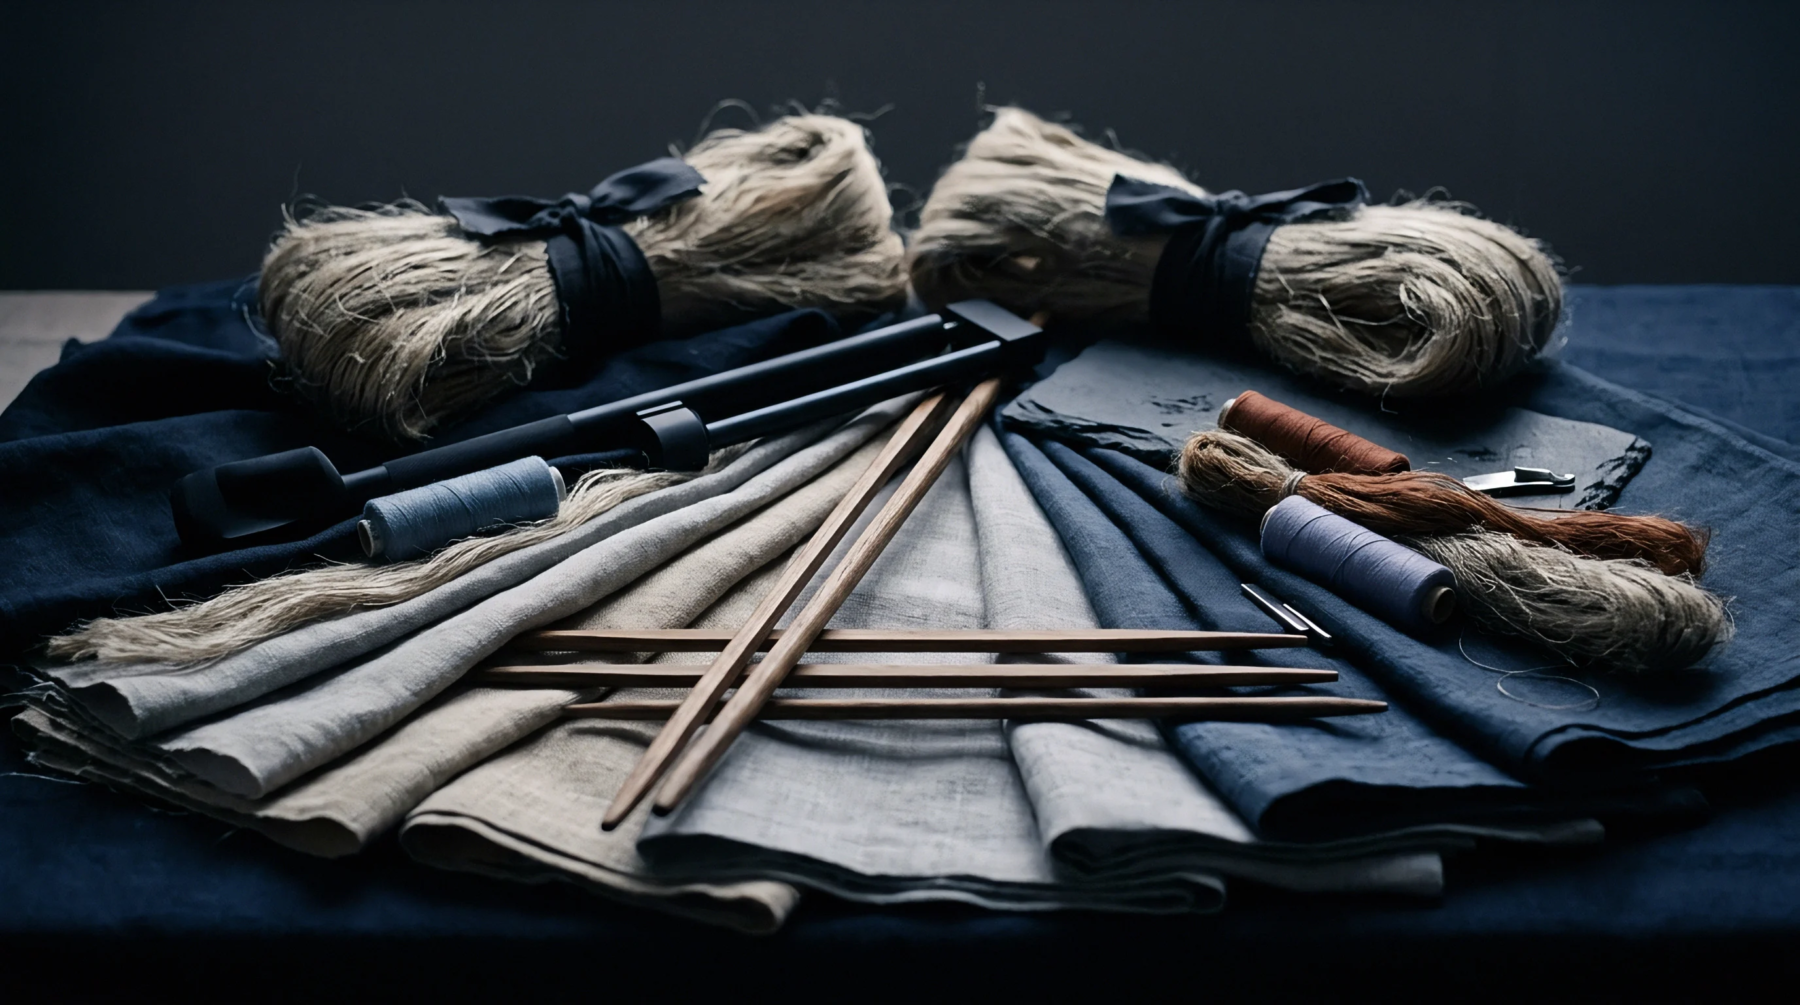
Professional fibre evaluation denotes the length of flax stalks following their mechanical extraction from the raw plant stems while keeping the individual bundles parallel to one another. Industry specialists classify long line flax as the primary output from the scutching process where the longest individual fibres remain unbroken during the removal of woody matter. Mills measure these fibres according to their reach, strength and cleanliness levels to determine their suitability for fine spinning lines.
Quality control teams compare batches against mill benchmarks that dictate the acceptable percentage of shorter tow fibres remaining in the lot. This raw material provides the material base for high count yarns where consistent length prevents breakage during high tension drafting. Producers document the physical dimensions of these fibre bundles in shipping manifests to satisfy the contract specifications held by spinning houses.
Processing Metric
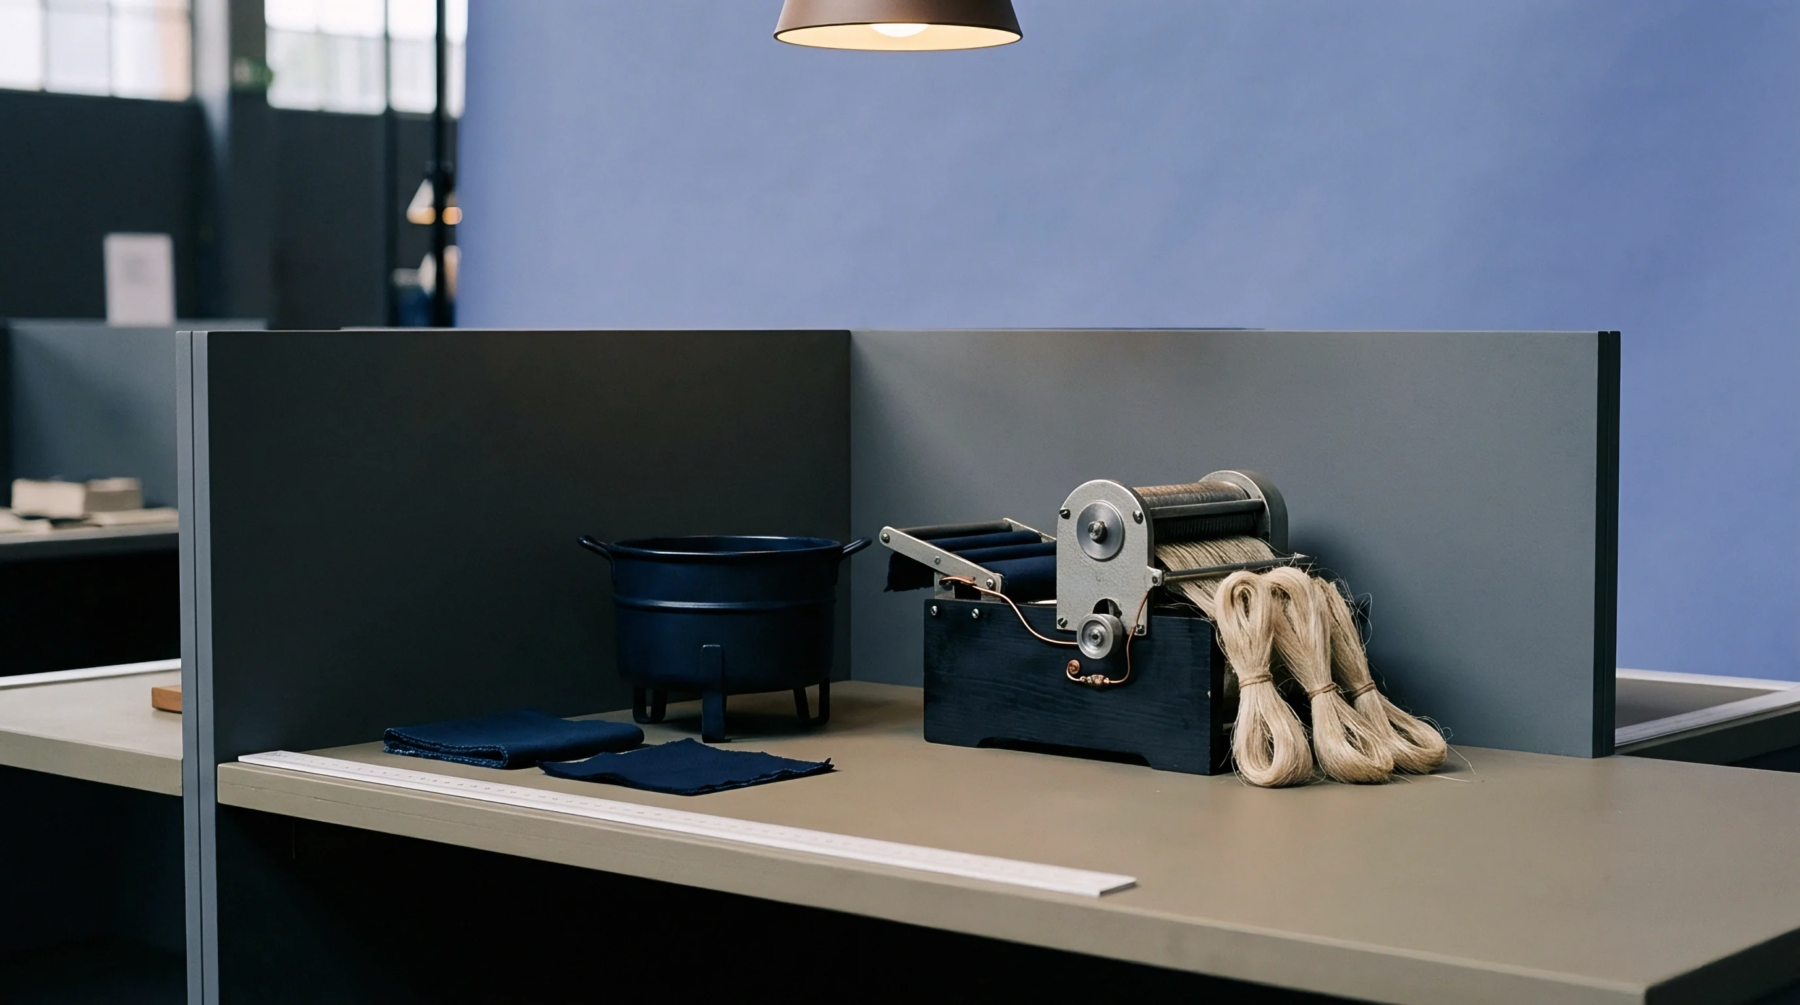
Moisture content influences the handling of long line flax during the combing phase at the factory floor. Machines pull these bundles through graduated sets of metal teeth to parallelise the constituent strands and remove remaining plant debris. Operatives maintain the alignment of these segments to ensure the final product retains its tensile properties for the production of apparel fabrics.
Variability in these measurements dictates the subsequent speed of the spinning frames and the final count of the produced yarn. Proper care during this stage prevents the snapping of individual strands that would otherwise weaken the finished yarn structure. Spinning facilities adjust their machinery settings based on the average measurement recorded for the specific batch entering the production line.
Contractual Specification
Quality assessments distinguish these bundles from standard tow products through a check of the average staple length and the absence of knotting. Buyers define the tolerance for defects such as impurities or broken fibres within their purchasing agreements to ensure consistent performance during weaving. Export documentation lists these grades according to the mill assessment to confirm that the delivery matches the internal processing requirements of the buyer.
A deviation from the stipulated length measurements triggers a price adjustment or the rejection of the shipment upon delivery. Precise fibre length remains the primary factor governing the mechanical efficiency of the mill.