Optimizing Warp Preparation Parameters for High Count Linen Yarns
Control unwinding tension below 12 cN, apply 12% modified starch-PVA size at 35 mPa·s, and beam at 70 Shore D with 8% moisture to maintain shed efficiency.
Control unwinding tension below 12 cN, apply 12% modified starch-PVA size at 35 mPa·s, and beam at 70 Shore D with 8% moisture to maintain shed efficiency.
Measure flax wet pick up through mass balance and microwave attenuation to maintain thirty percent dry size add-on.
Cut length density variance destabilizes wet drafting by altering dynamic friction in the trough, demanding precise ratch, saddle pressure, and thermal control.
Optimizing wet-spun high-count linen requires scoured line sliver under 1.2 dtex, strict 70°C trough water, precise 60mm ratch, and controlled balloon tension.
Compacting fine linen damasks demands 14-18% moisture, 135-145°C drum heat, and 2.2-3.4 kN/cm nip load to hold residual warp shrinkage under 2% without fibre damage.

Polymer clamp degradation causes dynamic slip and weft transfer failure at high picks per minute, demanding hydrolysis-resistant inserts and scheduled renewal.
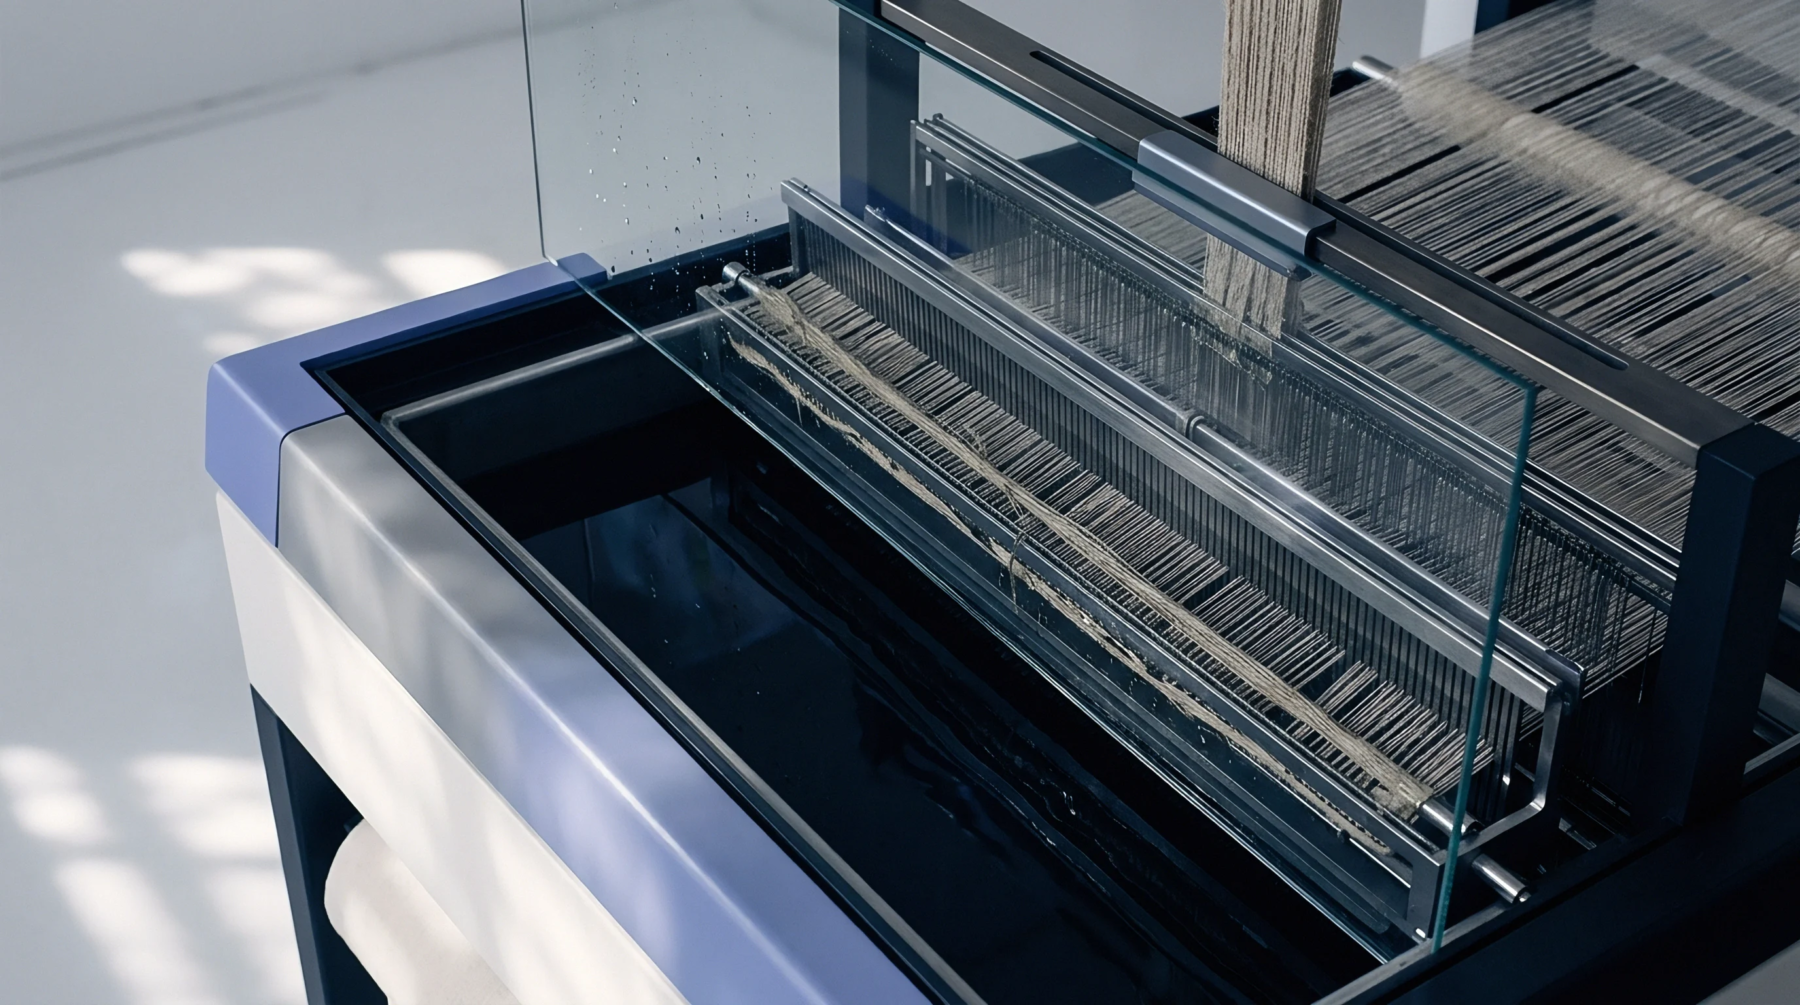
Controlled PVA sizing bounds radial penetration between fifteen and twenty-five percent, preserving internal flax flexibility while suppressing shed abrasion.
Warp sizing requires matching yarn packing factor to polymer viscosity, adjusting squeeze nip pressure for precise solids add-on, and maintaining elongation.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.