Drafting Mechanics
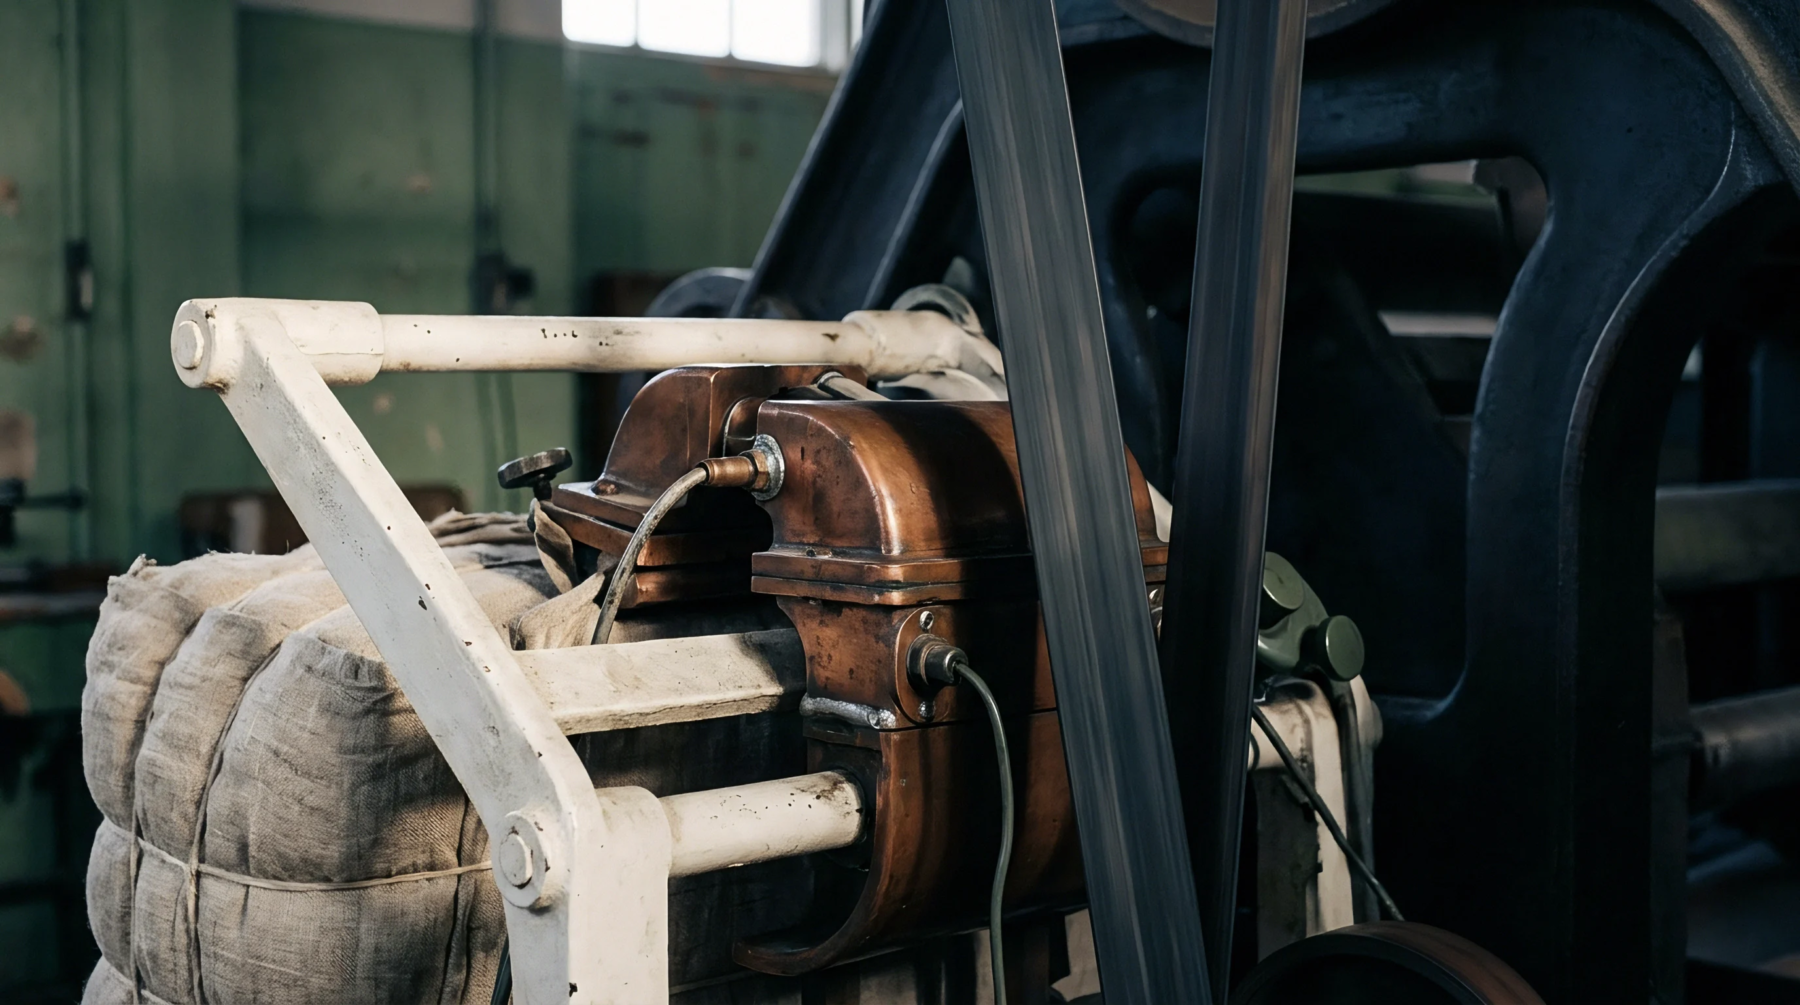
Flax preparation relies upon heavy draft operations where long-staple slivers undergo mechanical drafting inside an intersecting gill box to straighten stray fibres before spinning proceeds. Two pinned faller bars move faster than the feed rollers, drawing the material forward while pins pierce the mass to control the release speed of individual filaments. Short fibres receive insufficient pin engagement, creating uneven sliver density that subsequently triggers yarn breakage on ring frames.
Mill floor supervisors record these drafting irregularities on daily production sheets to separate internal processing standards from buyer acceptance criteria.
Pin Density
Pin density governs how effectively steel needles penetrate dense ribbon sheets without splitting individual flax stems during the drawing stroke. High pin concentrations distribute drafting resistance evenly across heavy slivers, preventing localized tearing that ruins batch tensile strength. Technicians calculate draft ratios by dividing output delivery speed by input feed speed, ensuring mechanical settings match the specific moisture regain of the flax material.
When moisture levels drop below standard thresholds, static electricity accumulates around the pin bars and draws loose lint toward moving mechanical parts.
Clearance Calibration
Mechanical clearance between faller bar screws and front delivery rollers determines the precise length over which drafting forces act on the sliver. Operators adjust this distance using feeler gauges during morning equipment checks to eliminate excessive fibre breakage before roving packages reach the wet spinning frames. Incorrect spacing allows clumps of flax to pass unmeasured, creating thick spots that violate export fabric grade tolerances recorded in final mill certificates.
Finished yarn regularity depends entirely upon maintaining this mechanical separation throughout continuous three-shift production cycles.