Conversion Accounting
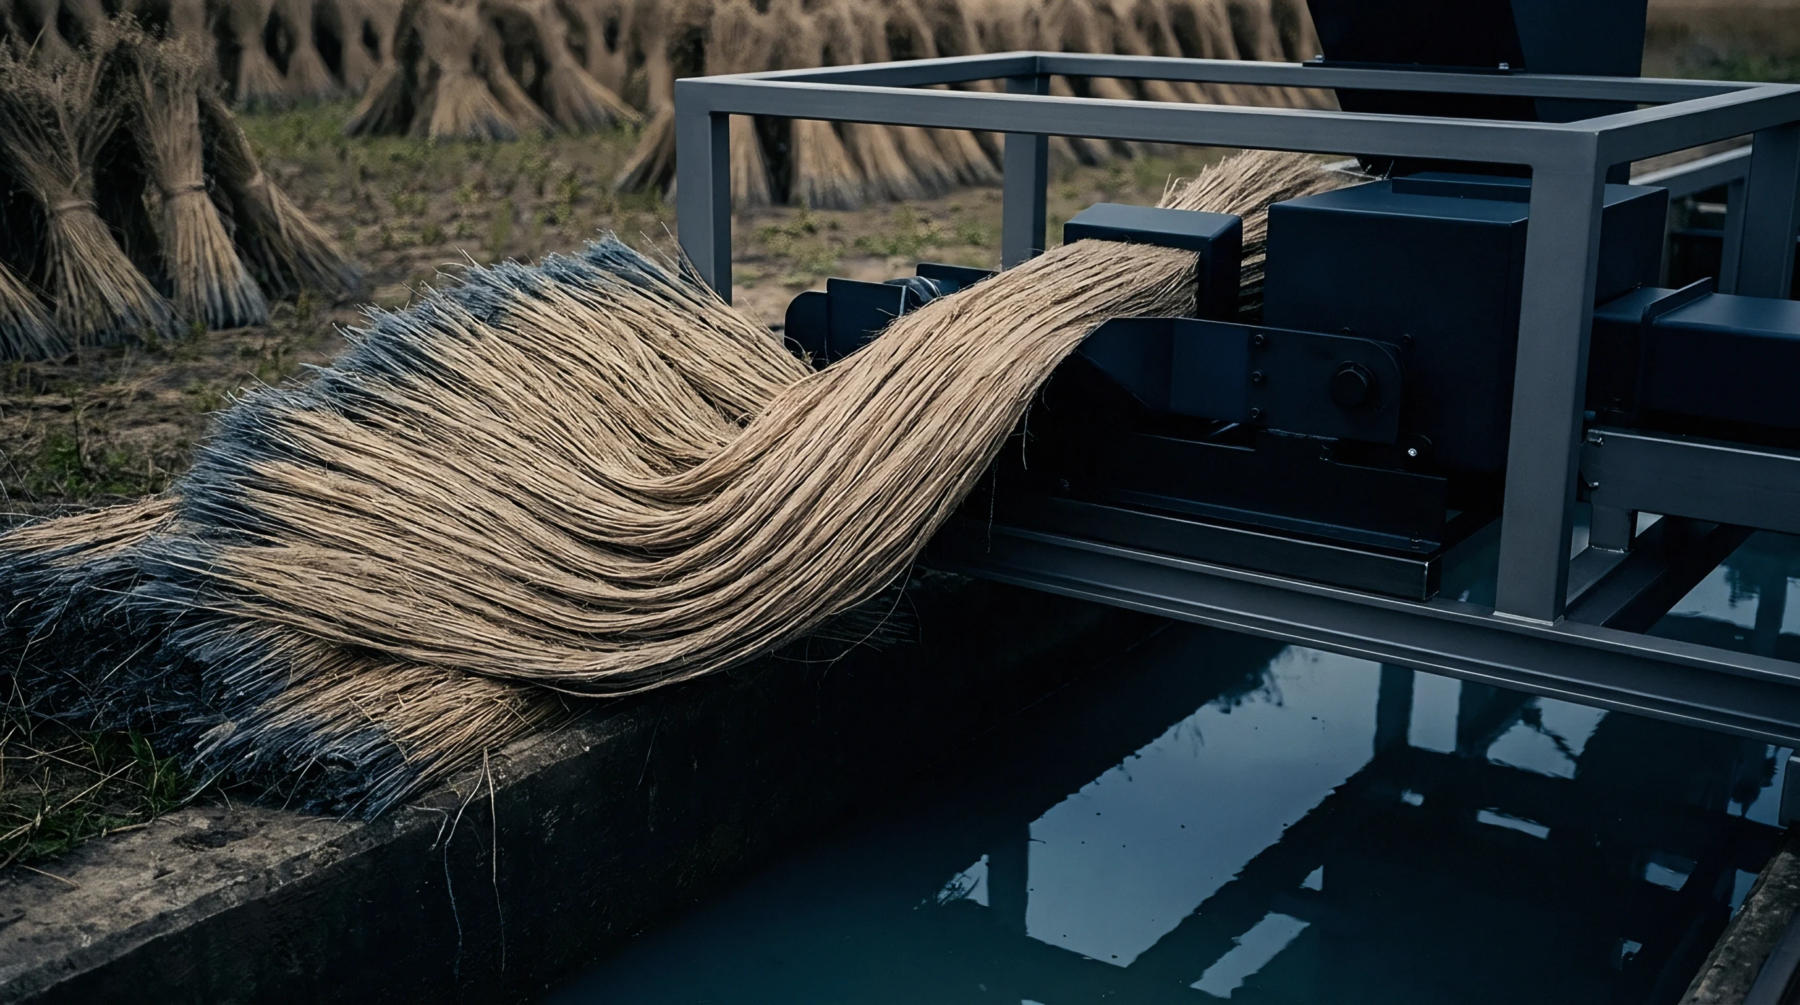
The financial reconciliation of raw flax mass to finished linen output constitutes toll manufacturing yield within our spinning mill accounting ledger. Mill supervisors track this specific transformation ratio during the wet spinning stage where long line flax fibres enter conversion processing and emerging wet spun yarn leaves the drafting frames. Raw material loss occurs during hackling and combing when short tow fibres separate from line fibre bundles, alongside moisture loss through controlled evaporation and occasional drafting breakage on the wet frames.
Buyers evaluate finished yarn deliveries against agreed contract tolerances, whereas mill operators monitor the conversion ratio to control variable processing costs. Excess material loss exceeding contractual allowances triggers financial adjustments on the monthly billing invoice sent to the merchant who supplied the raw flax straw.
Drafting Loss
Mechanical limitations on wet spinning frames restrict continuous output because roving breaks require piecing up by operators. Fine linen yarn production demands high tension on drafting rollers, which strains wet flax fibres and produces broken filaments that fall as waste beneath the machinery floor. Wet spinning yields depend directly on water temperature and immersion time within the hot water troughs because thermal conditioning softens natural pectins binding the elementary flax cells together.
Operators adjust twist levels to balance yarn strength against production speed, since excessive twist reduces overall output efficiency while insufficient twist increases breakage frequency during subsequent bobbin winding.
Export Measurement
Finished linen fabric inspection relies on mass balance calculations performed before goods receive export clearance stamps on the commercial shipping docket. Quality inspectors weigh the woven cloth rolls against the original dry weight of yarn issued to the weaving floor, after accounting for moisture regain standards specified in international flax trade rules. Fabric density grades differ from raw fibre grades because weaving introduces sizing compounds that add temporary weight before final scouring removes them during finishing.
Mill standards demand tighter conversion tolerances for export contracts than local market orders require, reflecting the strict quality thresholds enforced by overseas buyers.