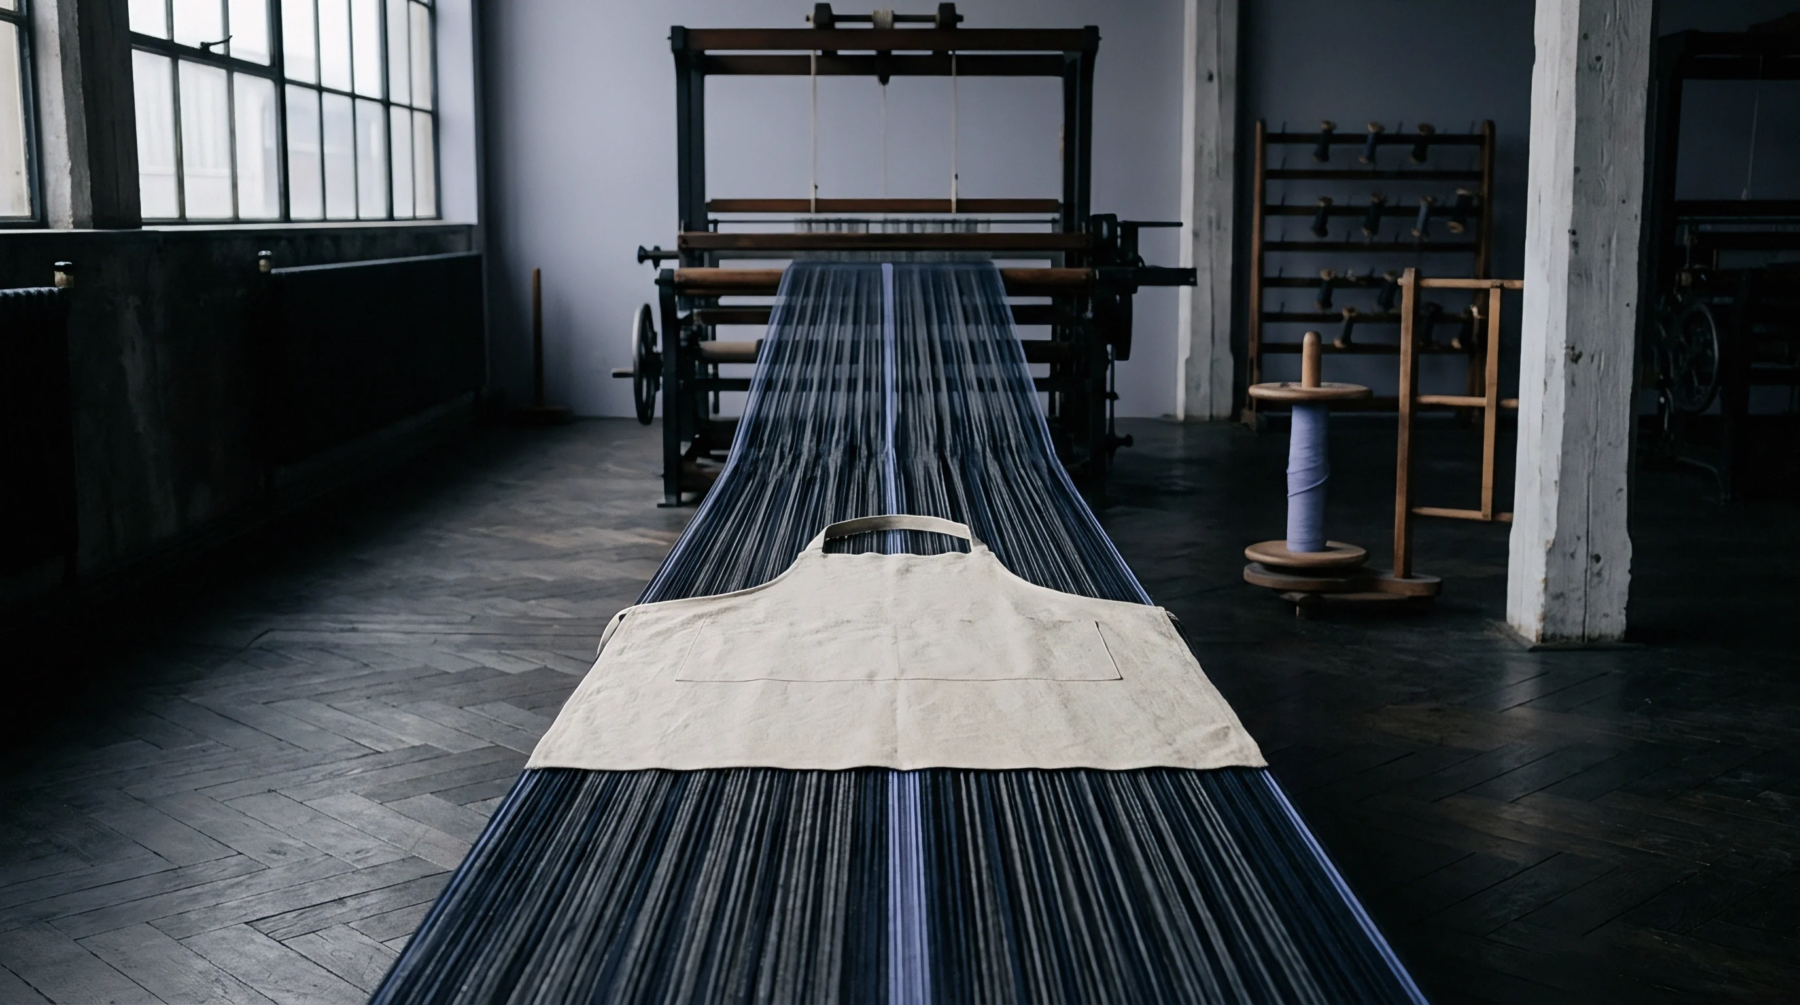
Mechanical Buffer
High speed loom operation requires the immediate regulation of warp drag forces to prevent yarn breakage at the moment of shed formation. tension peak reduction functions as an automated adjustment protocol during the weaving stage to distribute mechanical load across individual fibre strands. The controller monitors digital signals from the let off motor and modifies torque outputs to dampen excessive force spikes caused by rapid harness motion. Factory specifications designate this activity as the primary safeguard for warp integrity before the woven cloth reaches the inspection table.
It regulates the maximum allowable force applied to warp ends during high frequency insertion cycles and stops operation if the tension limits are exceeded. The mill record of these adjustments acts as a quantitative audit trail for assessing structural consistency of the final fabric.
Process Limit
Warp yarns undergo severe fatigue when tension peaks are not smoothed during the opening and closing of the shed. tension peak reduction manages this stress by slowing the release of the warp beam at the exact millisecond the harness reaches its maximum displacement. Without this intervention, fine flax yarns snap frequently and necessitate lengthy machine downtime to repair individual breaks. Skilled weavers verify that the automated compensation prevents uneven density throughout the length of the fabric roll.
Each mill applies specific thresholds based on the fibre quality grade and the yarn count currently on the loom. A higher grade of flax fibre tolerates greater mechanical force but still benefits from controlled load management to maintain uniform finish quality. Management of these brief force cycles determines the difference between consistent output and frequent stop-start production failures.
Audit Protocol
Quality assurance teams perform spot checks on the digital logs to ensure that the tension peak reduction remains active during heavy-duty production runs. Operators compare the automated logs against the fabric defect report to identify any correlation between unadjusted tension spikes and local weave faults. Accurate documentation of load peaks allows the facility to refine the loom settings for future orders with similar raw material specifications.
The absence of these logs signifies an unverified production line where structural integrity remains uncontrolled throughout the manufacturing sequence. Verified peak data provides the only reliable evidence of consistent stress management in high speed weaving.