Tension Variance
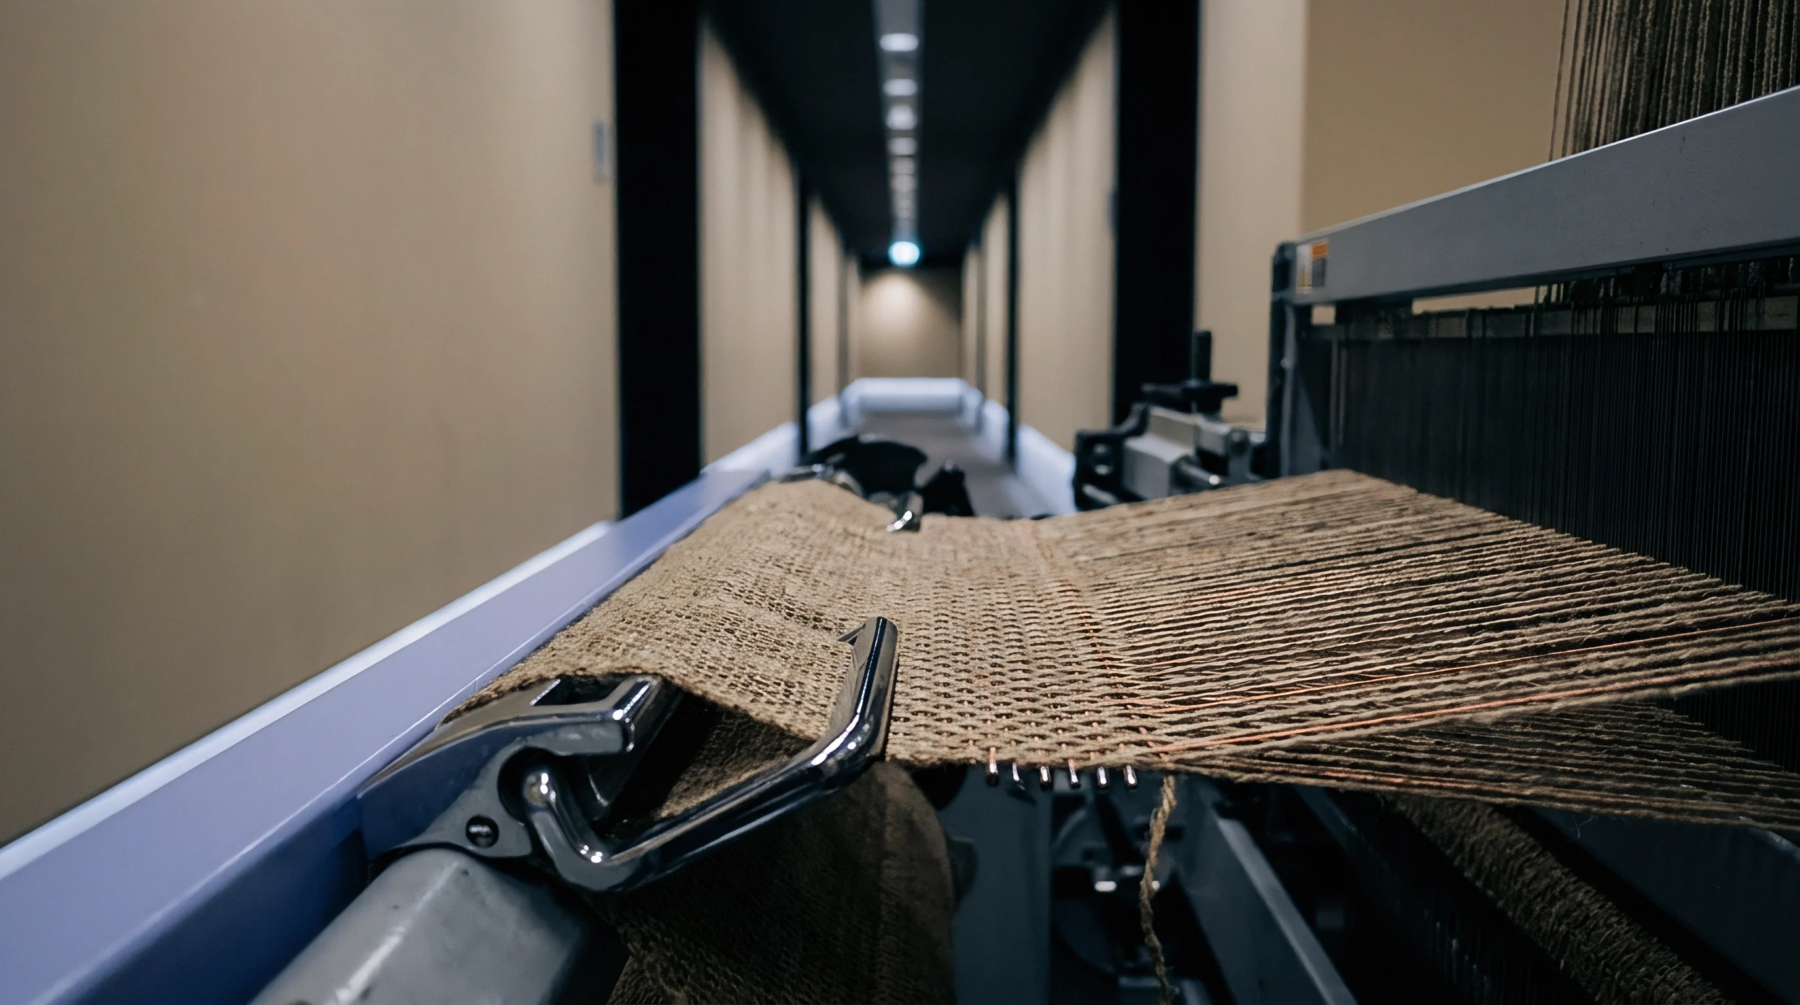
High-speed loom performance depends on the controlled physical resistance of longitudinal yarns against the harness mechanisms. The linen warp cling phenomenon occurs when electrostatic friction or surface hairiness causes adjacent warp ends to adhere during the shed opening cycle. This technical defect prevents the clear separation of the warp sheet, resulting in skipped picks or broken filaments that necessitate an immediate halt of the weaving process.
Mills calculate this resistance by measuring the force required to lift the top shed against the internal friction of the yarn pack.
Application Threshold
Quality control personnel monitor this force during the primary inspection phase before the loom beams move to the weaving hall. Acceptance criteria typically dictate that the force must remain beneath the mill threshold to prevent uneven fabric density or reed marks. Records of these measurements appear in the production log for each loom beam, which provides traceability from the initial dressing station back to the yarn sizing unit.
Disparities between the mill standard and the buyer criteria for finish often lead to specific rejections when the cling exceeds the tolerance for high-density luxury goods.
Mechanical Consequence
Fibres lacking adequate sizing agents show a greater tendency toward entanglement because the dry surface area permits increased inter-fibre locking. Proper application of starch or synthetic binders during the slashing stage creates a protective film that masks the natural tendency of the flax fibre to bond with its neighbors. Variations in ambient humidity levels inside the production area alter the surface charge, which further exacerbates the unwanted adhesion between yarns during the rapid vertical movement of the harness frames.
Consistent moisture regulation at the point of weaving ensures the stability of the warp path and prevents the mechanical strain that ruins the uniformity of the final cloth.