Doubling Sequence
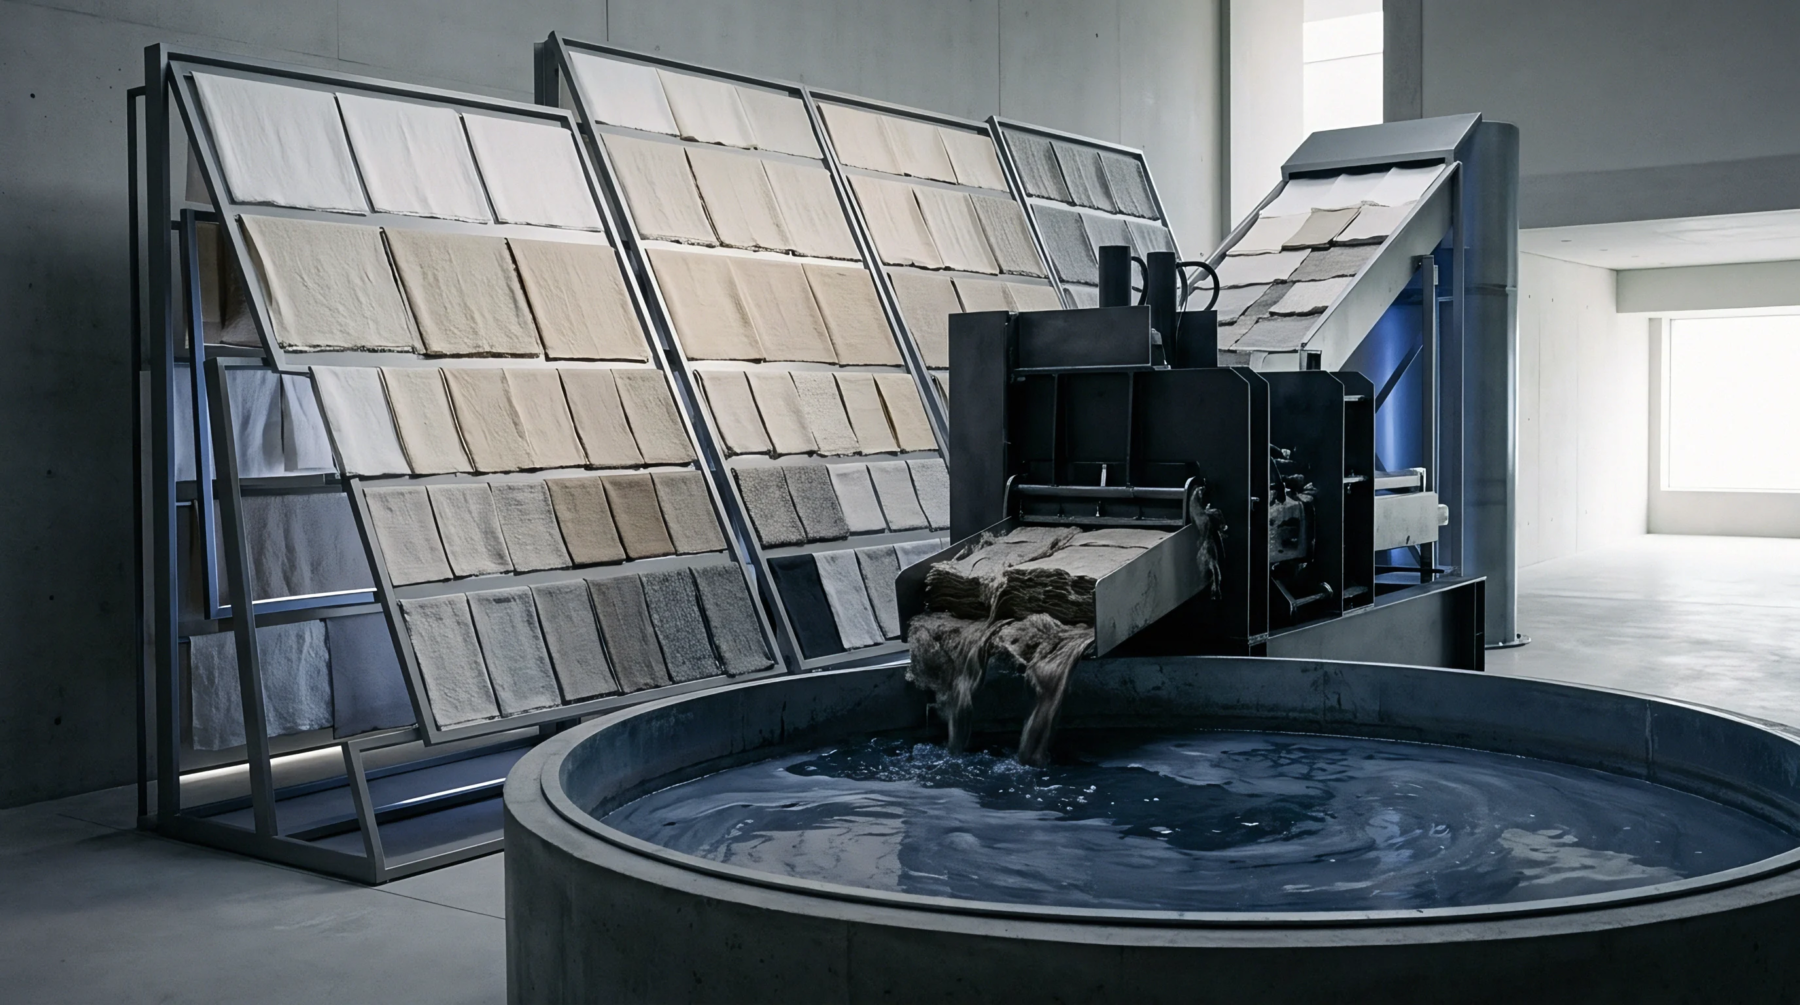
Sequential combining and attenuating of multiple flax slivers improves linear density uniformity and aligns short bast fibers along the strand axis. Performed on draw frames across multiple passages in flax spinning mills, sliver drawing reduces mass variation through doubling while drafting the combined strand back to target linear mass. Machine setup documents record draft ratios and doubling counts for each passage stage.
Combining four to eight slivers averages out mass irregularities present in individual feeding strands. The process operates strictly on unspun fiber strands before twist insertion on roving or spinning frames.
Roller Speed
Differential surface speeds between back and front drafting rollers stretch the fiber mass to attenuate the sliver. Faller pins or control aprons maintain tension on short flax fibers during drafting to prevent unguided fiber clumps from moving into the front nip. Incorrect roller gauge settings cause fiber breaking or uncontrolled drafting waves in the output sliver.
Regular maintenance of rubber roller cots prevents surface grooving and inconsistent nip pressure.
Mass Uniformity
Drawing passage targets enforce strict delivery sliver weight tolerances within one percent of target mass per meter. Exceeding mass variation limits requires immediate machine stopping and re-pinning of faller field zones.