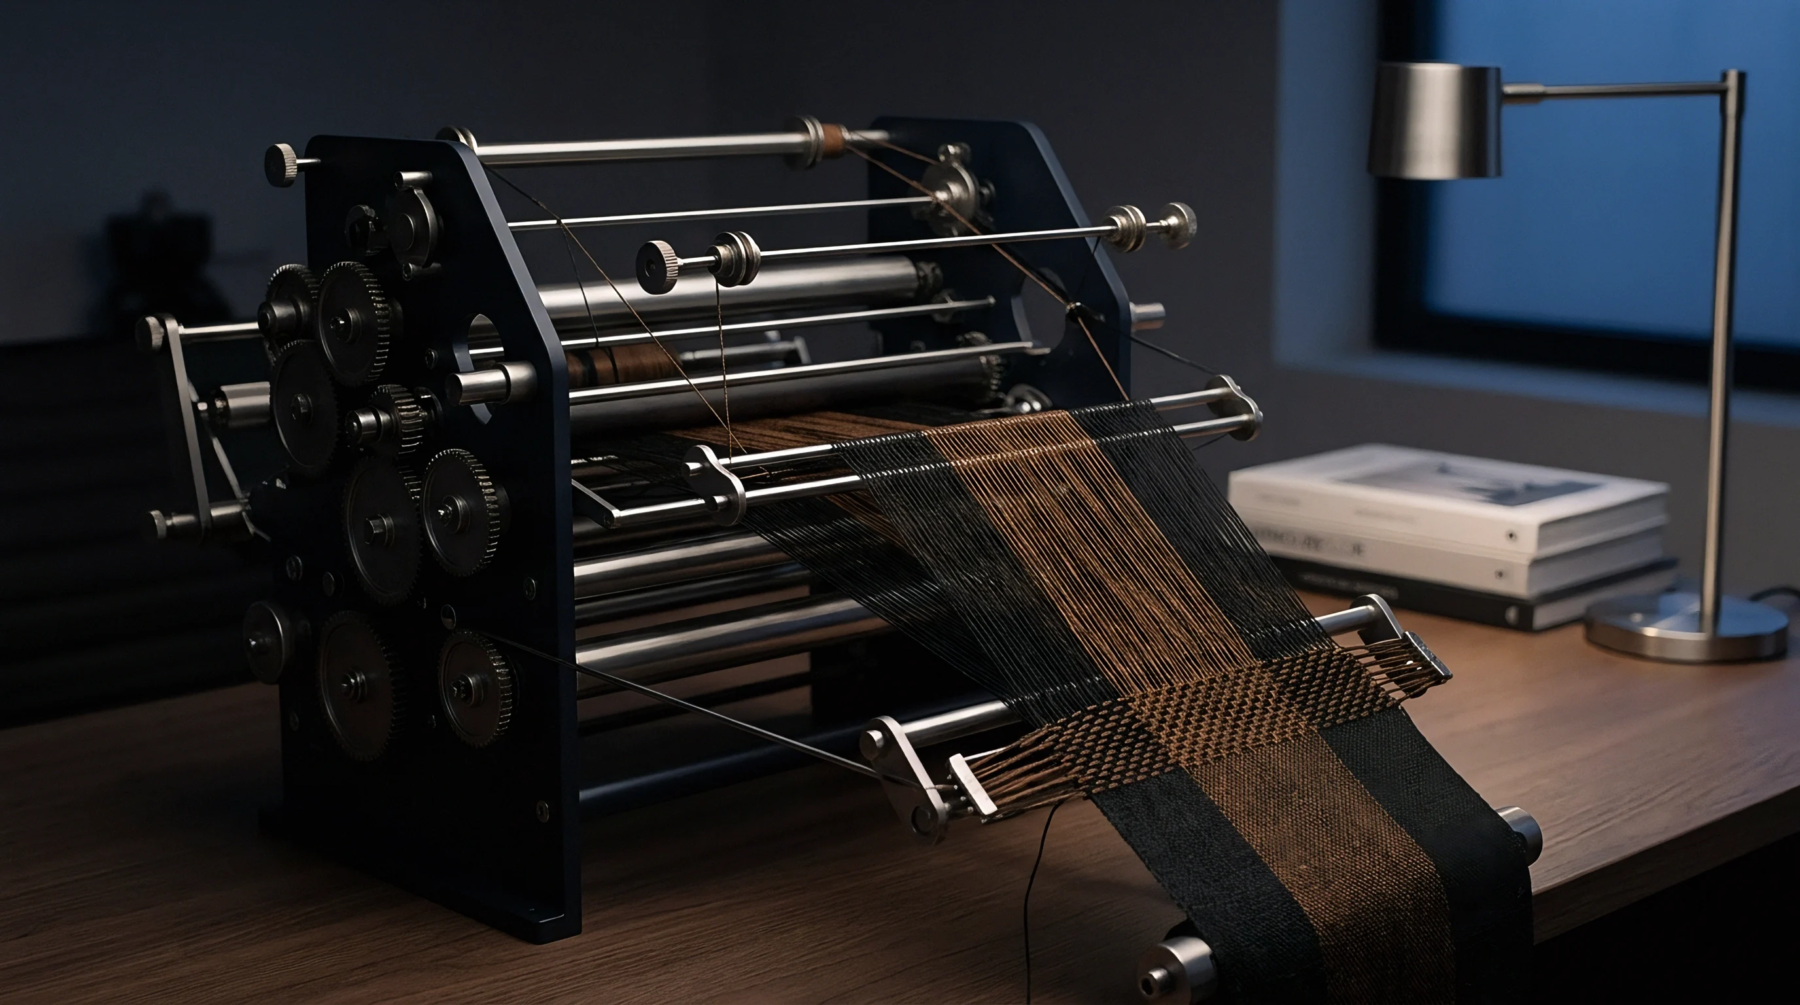
Loom Architecture
Mechanical limitations in Chinese flax weaving dictate that reed width constraints restrict the maximum achievable width of unstitched linen fabric on the loom. Mechanical designers set these boundaries based on the physical deflection limits of the sley and the shedding mechanism. Heavier yarn counts demand wider dent spacing, reducing the total ends per inch available across the span.
Production planners record these fixed parameters in the factory setup sheet before yarn goes to the beam. Exceeding the spatial limits causes warp tension imbalances and immediate thread breakage during operation.
Beam Allocation
Mill operators prevent mechanical failure during production by aligning yarn density with the physical parameters defined by reed width constraints. Flax spinning mills supply warps that must match the dent wire count without bunching or crossing over the metal blades. Quality inspectors verify the beam width against the loom specifications before the mounting process begins in the weaving shed.
Fabric grades depend on this initial alignment because uneven dent distribution creates permanent streaks in the finished cloth.
Export Clearance
Export inspectors evaluate finished linen goods against global buyer acceptance criteria rather than internal mill benchmarks. Commercial contracts specify maximum allowable widths, and shipments failing to meet these numerical limits incur financial penalties from the purchasing house. Customs documentation records the verified dimensions of the rolled bolts before they leave the bonded warehouse for international transport.
Final trade agreements rely on these verified measurements to determine whether the delivered consignment satisfies the commercial requirements.