Energy Intensity
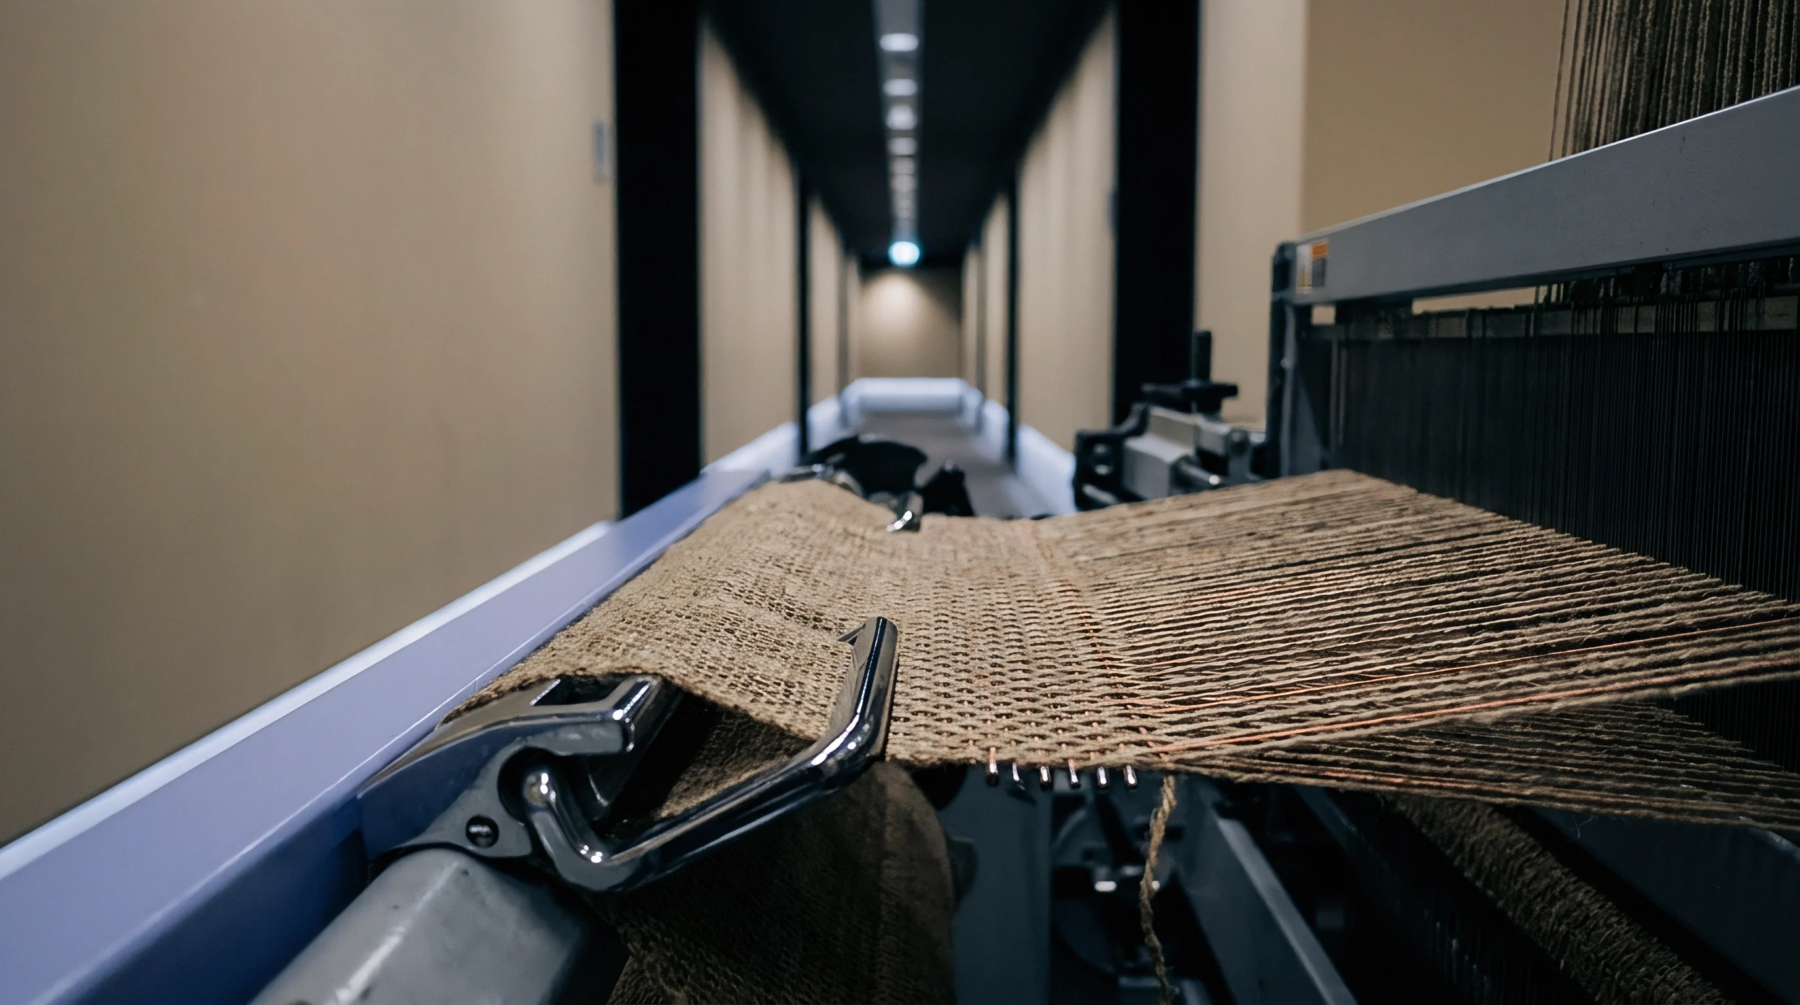
Electrical power consumption per unit of linear output characterizes the operational efficiency of industrial machinery. A kilowatt-hour per meter quantifies the amount of electricity consumed to process a single meter of linen fabric or yarn during a production cycle. Spinning frames and weaving looms utilize this metric to establish baseline performance expectations during high-volume manufacturing.
Management teams record these values in the daily energy log to monitor how electrical loads fluctuate across different production lines. Variations in drive motor torque or friction within the heavy-duty transmission components alter the energy required for each meter of output. Stable electricity usage per meter indicates mechanical consistency while spikes suggest either machine wear or excessive tension in the textile material.
Consumption Calculation
Engineers determine the specific draw by dividing the total active energy recorded at the machine intake over a defined interval by the linear length of the product processed. This ratio accounts for the auxiliary equipment connected to the main production circuit such as suction systems for dust removal or electronic sensors for break detection. Measuring this performance metric requires high-precision power analyzers mounted at the distribution board of the weaving shed.
Frequent sampling of the current draw during the entire cycle captures both the constant running load and the energy spikes occurring during start-up or loom stop events. A lower kilowatt-hour per meter value signifies that the motor utilizes power efficiently to overcome inertial resistance rather than losing energy through heat or vibration.
Verification Protocol
Procurement contracts often include maximum allowable energy limits per unit to ensure that the supplier maintains efficient machinery. Compliance requires the mill to submit monthly reports detailing the average kilowatt-hour per meter for every production batch. Auditors review these records against internal factory benchmarks to verify if the machinery performs within the designed operational parameters.
Discrepancies between the recorded value and historical machine output act as a diagnostic signal for maintenance interventions. High electrical consumption relative to previous batches points toward mechanical misalignment or degraded drive belts that increase the mechanical impedance of the system. Operational energy data provides a verifiable link between factory equipment status and the final cost of the textile output.