Motion Mechanics
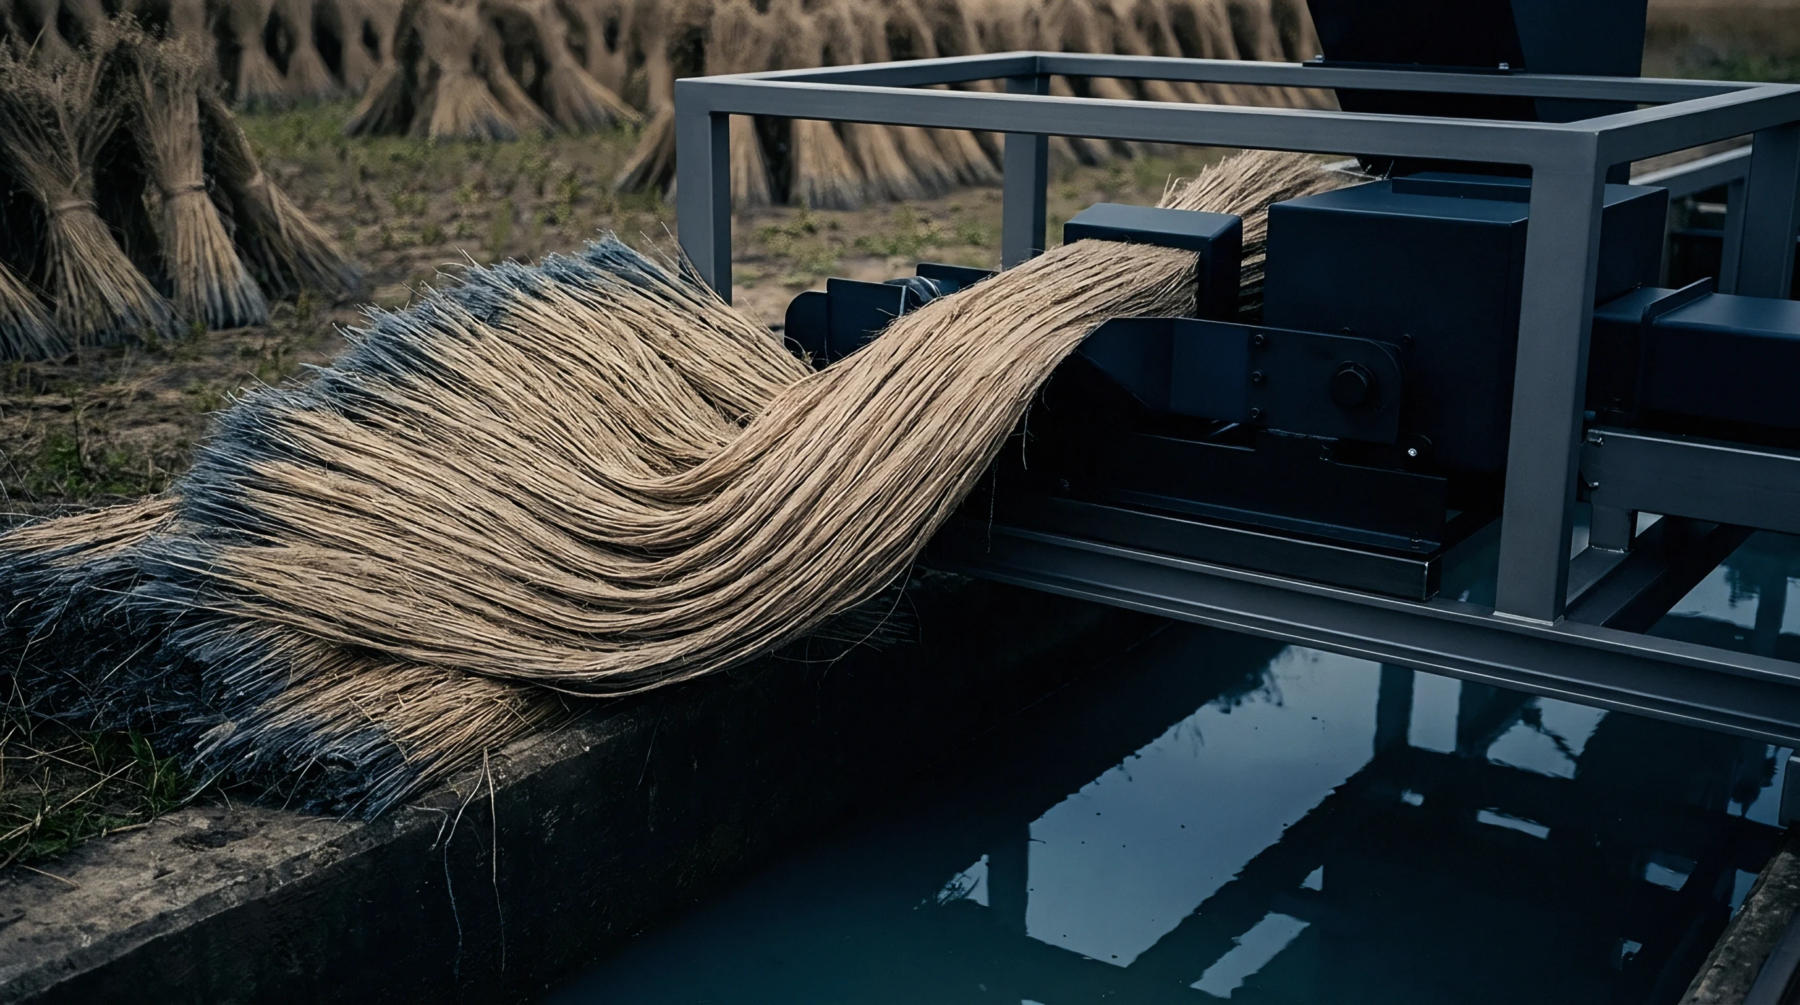
Drawing zone mechanical operations govern the rate of attenuation and fibre alignment during yarn production. Within flax spinning frames, drafting kinetics describes the speed differentials, acceleration zones and frictional forces acting on sliver bundles. High draft ratios force fibre bundles to accelerate from back roller velocity to front roller velocity over a short distance.
Mill technical sheets specify nip point pressures and roller surface characteristics to maintain control over moving fibres. Proper kinetic management prevents draft waves and thin places in the resulting linen yarn.
Velocity Difference
Acceleration profile parameters determine how individual flax fibres detach from the main strand mass. Fibres entering the draft field travel at slow back-roller surface speeds until front-roller nip forces pull them into high-speed zones. Variable fibre length in scutched flax creates unstable floating fibre movement between drafting rollers.
Apron control devices and pressing rollers exert surface friction to constrain premature movement of short fibres. Speed ratios between input and output rollers define the nominal draft factor recorded in spinning mill specifications. Uncontrolled velocity shifts generate mass variation, which appears as periodic thick and thin spots on yarn capacitive testing equipment.
Tension Limit
Inter-fibre friction inside the drafting zone creates resistance that limits maximum draft ratios. High strand tension leads to fibre rupture rather than slippage, increasing end-break rates on spinning frames. Process engineers balance moisture content and drafting speed to optimize fibre sliding without compromising yarn strength.