Production Constraint
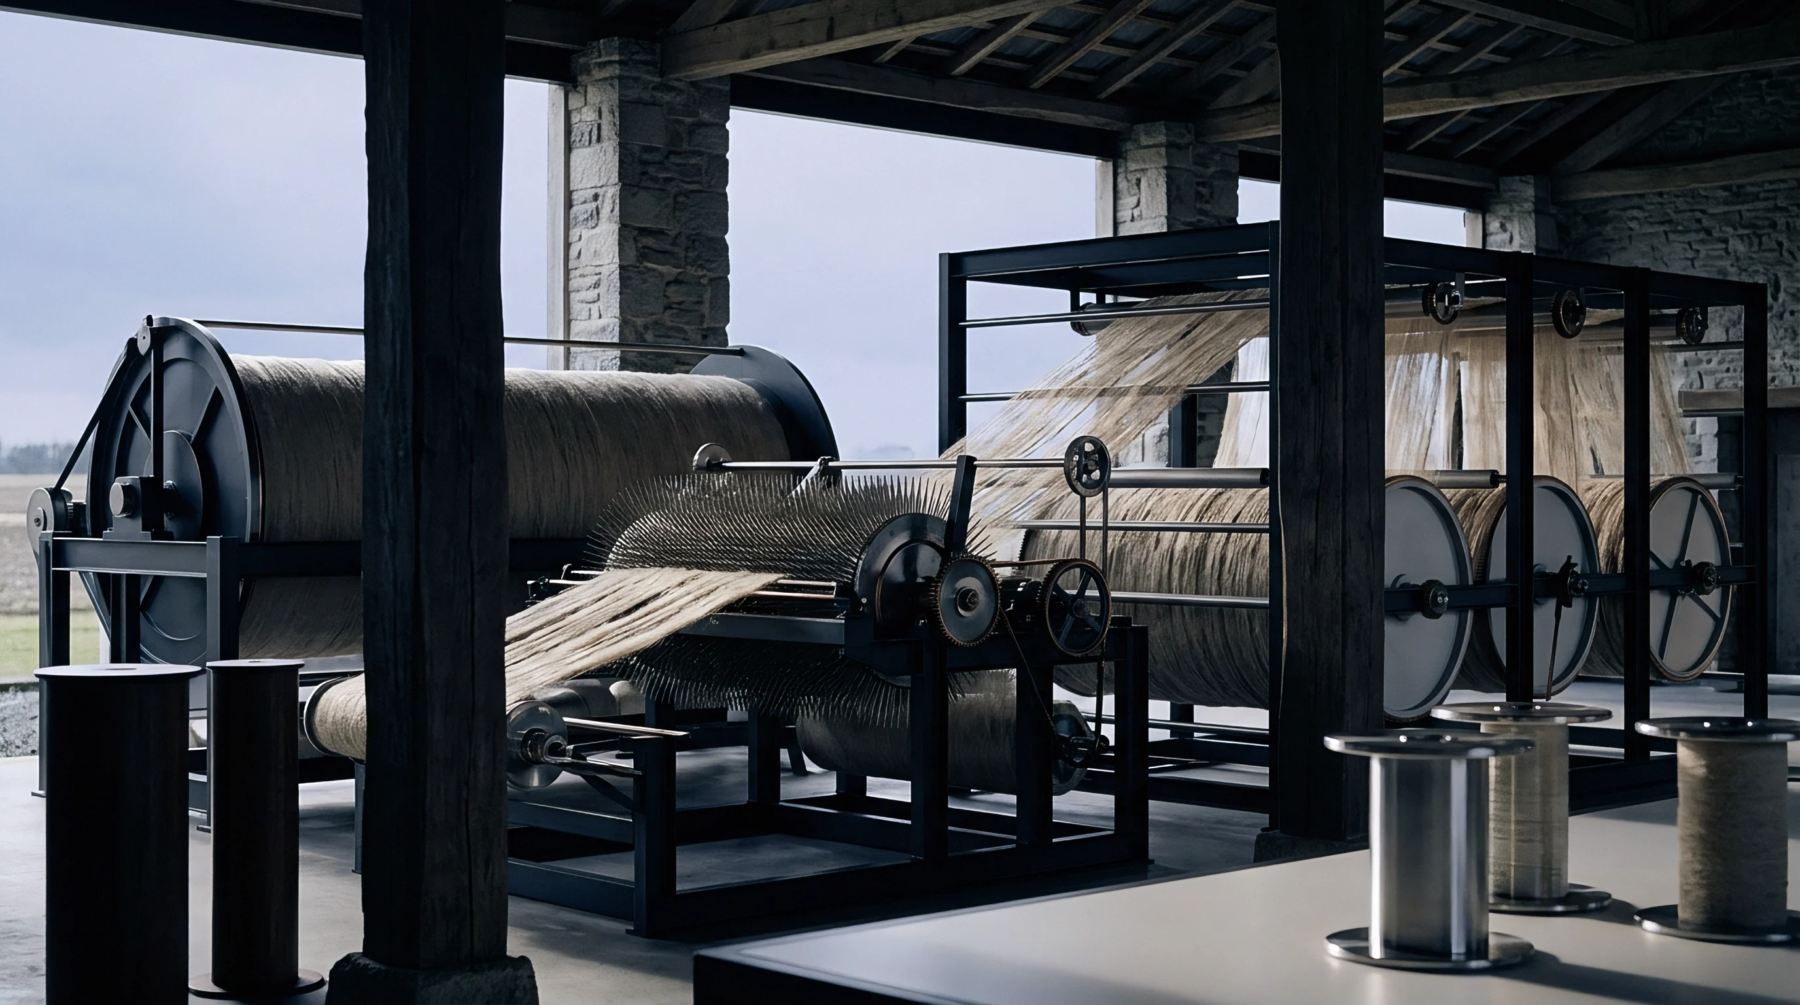
Mechanical platforms supporting the vertical pinned bars within flax gill boxes define drawing faller beds through their alignment and density. These drawing faller beds govern the attenuation of fibre slivers by ensuring that each individual pin maintains a constant depth within the material mass as the carriage transitions from the feed to the delivery rollers. The component limits the horizontal displacement of the bars during high speed operation.
Maintaining parallelism between the bed surface and the roller axis prevents irregular drafting in the spinning prep stage. Uniformity here dictates the regularity of the yarn weight per unit length across the entire production lot. Proper contact pressure reduces friction heat which protects the fibre from mechanical degradation during the combing process.
Maintenance Requirement
Precise calibration of these tracks occurs during scheduled downtime to address the gradual accumulation of linseed oil residue and microscopic debris. Technicians inspect the surface for pitting or uneven wear patterns that indicate misalignment in the carriage drive. Hardened steel inserts act as the primary contact surface to extend the interval between full overhauls.
Adjusting the clearance between the sliding bar ends and the lateral guides ensures the pins stay centered within the fibre path. Excessive clearance allows the bars to skew under tension and introduces periodic faults in the sliver consistency. Replacing worn components requires full machine shutdown because any variation in bed geometry alters the attenuation ratio immediately upon startup.
Consistent surface hardness ensures that high tension cycles do not deform the tracks over time.
Operational Variance
Quality control logs record the deviation from nominal bed height as a means of monitoring mechanical drift within the gill drawing frames. Each mill sets a tolerance range for the verticality of the pins based on the average staple length of the raw flax supply. Narrow margins assist in the production of fine count yarns while wider settings manage coarse fibres.
Buyers evaluate the consistency of the finished output against the mill standard recorded in the pre-shipment report. Minor inconsistencies in the bed settings correlate directly with variations in the coefficient of variation observed in the final spun product. Precision in this mechanism remains the primary determinant for the batch uniformity of the linen output.